
Self-Drilling Screws for Light-Gauge Steel Structures: Drill Point Selection, Thread Engagement, and Pull-Out Performance
Han Congming
AuthorWith experience in screw and fastener manufacturing and sales, we operate our own production facility with stable large-scale capacity. We are specialists in self-drilling screws, drywall screws, chipboard screws, machine screws, bolts, and customized fasteners for construction and industrial applications.
Connection Requirements for Self-Drilling Screws in Light-Gauge Steel Structures
Connection Characteristics of Light-Gauge Steel and Cold-Formed Thin-Walled Steel
With the development of prefabricated buildings, modular construction, and lightweight steel housing, light-gauge steel structures and cold-formed thin-walled steel structures are increasingly used for walls, roofs, partitions, and building envelope systems. Compared with heavy steel members, light-gauge steel components generally have thinner walls, lower self-weight, and a larger number of connection points. As a result, fasteners must provide sufficient strength while also supporting fast, continuous, and standardized installation.
In these structures, connection points may be exposed to tension, shear, wind loads, and repeated vibration during construction and service. If the screw does not form a stable connection, problems such as member displacement, panel loosening, or local deformation may occur. Therefore, light-gauge steel connections should not be evaluated only by whether the screw can penetrate the steel. Their long-term load-bearing capacity and durability must also be considered.
The Main Role of Self-Drilling Screws in Light-Gauge Steel Structures
Self-drilling screws use their own drill points to create holes and then form threads in the steel, reducing the need for a separate pre-drilling operation. In light-gauge steel construction, this connection method can improve installation efficiency and reduce positioning and drilling errors on site.
Industry terms such as light-gauge steel framing screws, self-drilling screws for light-gauge steel, and steel framing screws generally refer to fastening requirements for light-gauge framing, thin-walled steel members, wall panels, and roof-envelope systems. Their function is not limited to fixing two components together. They also transfer loads, limit member movement, and help maintain the overall stability of the building envelope.
Key Factors Affecting Connection Reliability
The main factors affecting connection reliability include:
- Steel thickness: determines the required drilling range of the drill point;
- Drill point type: affects drilling speed, penetration ability, and drilling stability;
- Thread engagement: determines whether the screw can form effective mechanical engagement with the steel;
- Installation torque: affects head clamping and thread load transfer;
- Load condition: different connection locations have different requirements for pull-out, shear, and pull-over resistance.
Therefore, the selection of self-drilling screws for light-gauge steel structures should focus not only on whether the screw can be installed, but also on whether it can form a reliable structural connection.
Drill Point Selection and Steel Thickness Matching
The Effect of Drill Point Type on Drilling Performance
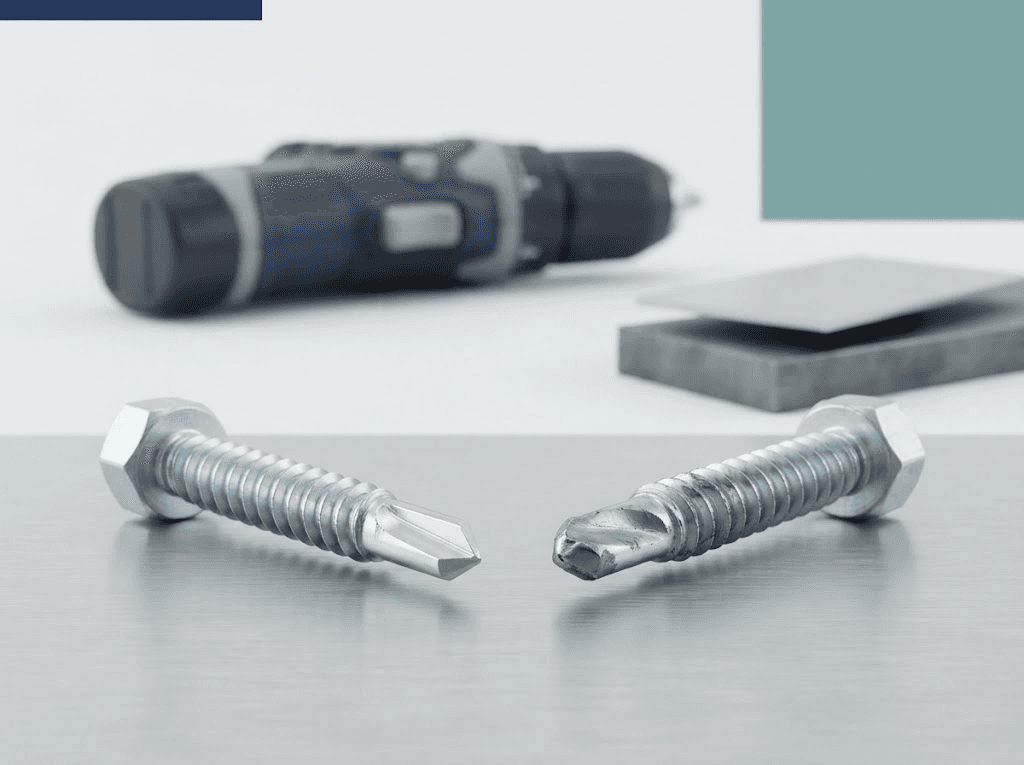
In industry search topics such as self-drilling screws for thin steel and self-drilling screws for thick steel, drill point selection is a central consideration. The length, diameter, cutting-edge geometry, and heat treatment of the drill point all affect the screw’s ability to penetrate steel.
If the cutting capacity is insufficient, the screw may slip on the steel surface, overheat, or break. When the drill point is properly matched to the steel thickness, the screw can complete drilling efficiently and create the conditions required for subsequent thread formation. The drill point is therefore not simply the end of the screw; it is a critical component that affects both installation efficiency and initial connection quality.
Selection Principles for Different Steel Thicknesses
For relatively thin light-gauge steel sheets, the drill point should provide flexible cutting and smooth chip evacuation, while avoiding unnecessary damage to the back side of the material after penetration. For multiple steel layers or thicker cold-formed members, a drill point with a greater drilling range and sufficient hardness should be selected.
The following factors should be considered together:
- The total thickness of single or multiple steel layers;
- Steel strength and hardness;
- The presence of coatings or surface treatments;
- Whether sufficient effective thread will remain after penetration;
- Whether the connection will be exposed to significant tension or shear.
In other words, drill point selection should not be based only on the overall screw length. It should be based on the total thickness of the materials being connected.
Problems Caused by Drill Points That Are Too Short, Too Long, or Too Soft
If the drill point is too short, the screw may not penetrate the full thickness of the steel, causing drilling to stop before the threads are fully formed. If the drill point is too long, it may complete the penetration but increase installation time and cause unnecessary local damage in thin-walled members.
If the drill point has insufficient hardness, drilling may become slow, the cutting tip may wear prematurely, and the screw may overheat or break. For structural self-drilling screws and connections involving thicker steel, drill point performance must be carefully matched to the steel thickness.
Thread Engagement and Connection Strength
The Importance of Effective Thread Engagement Length
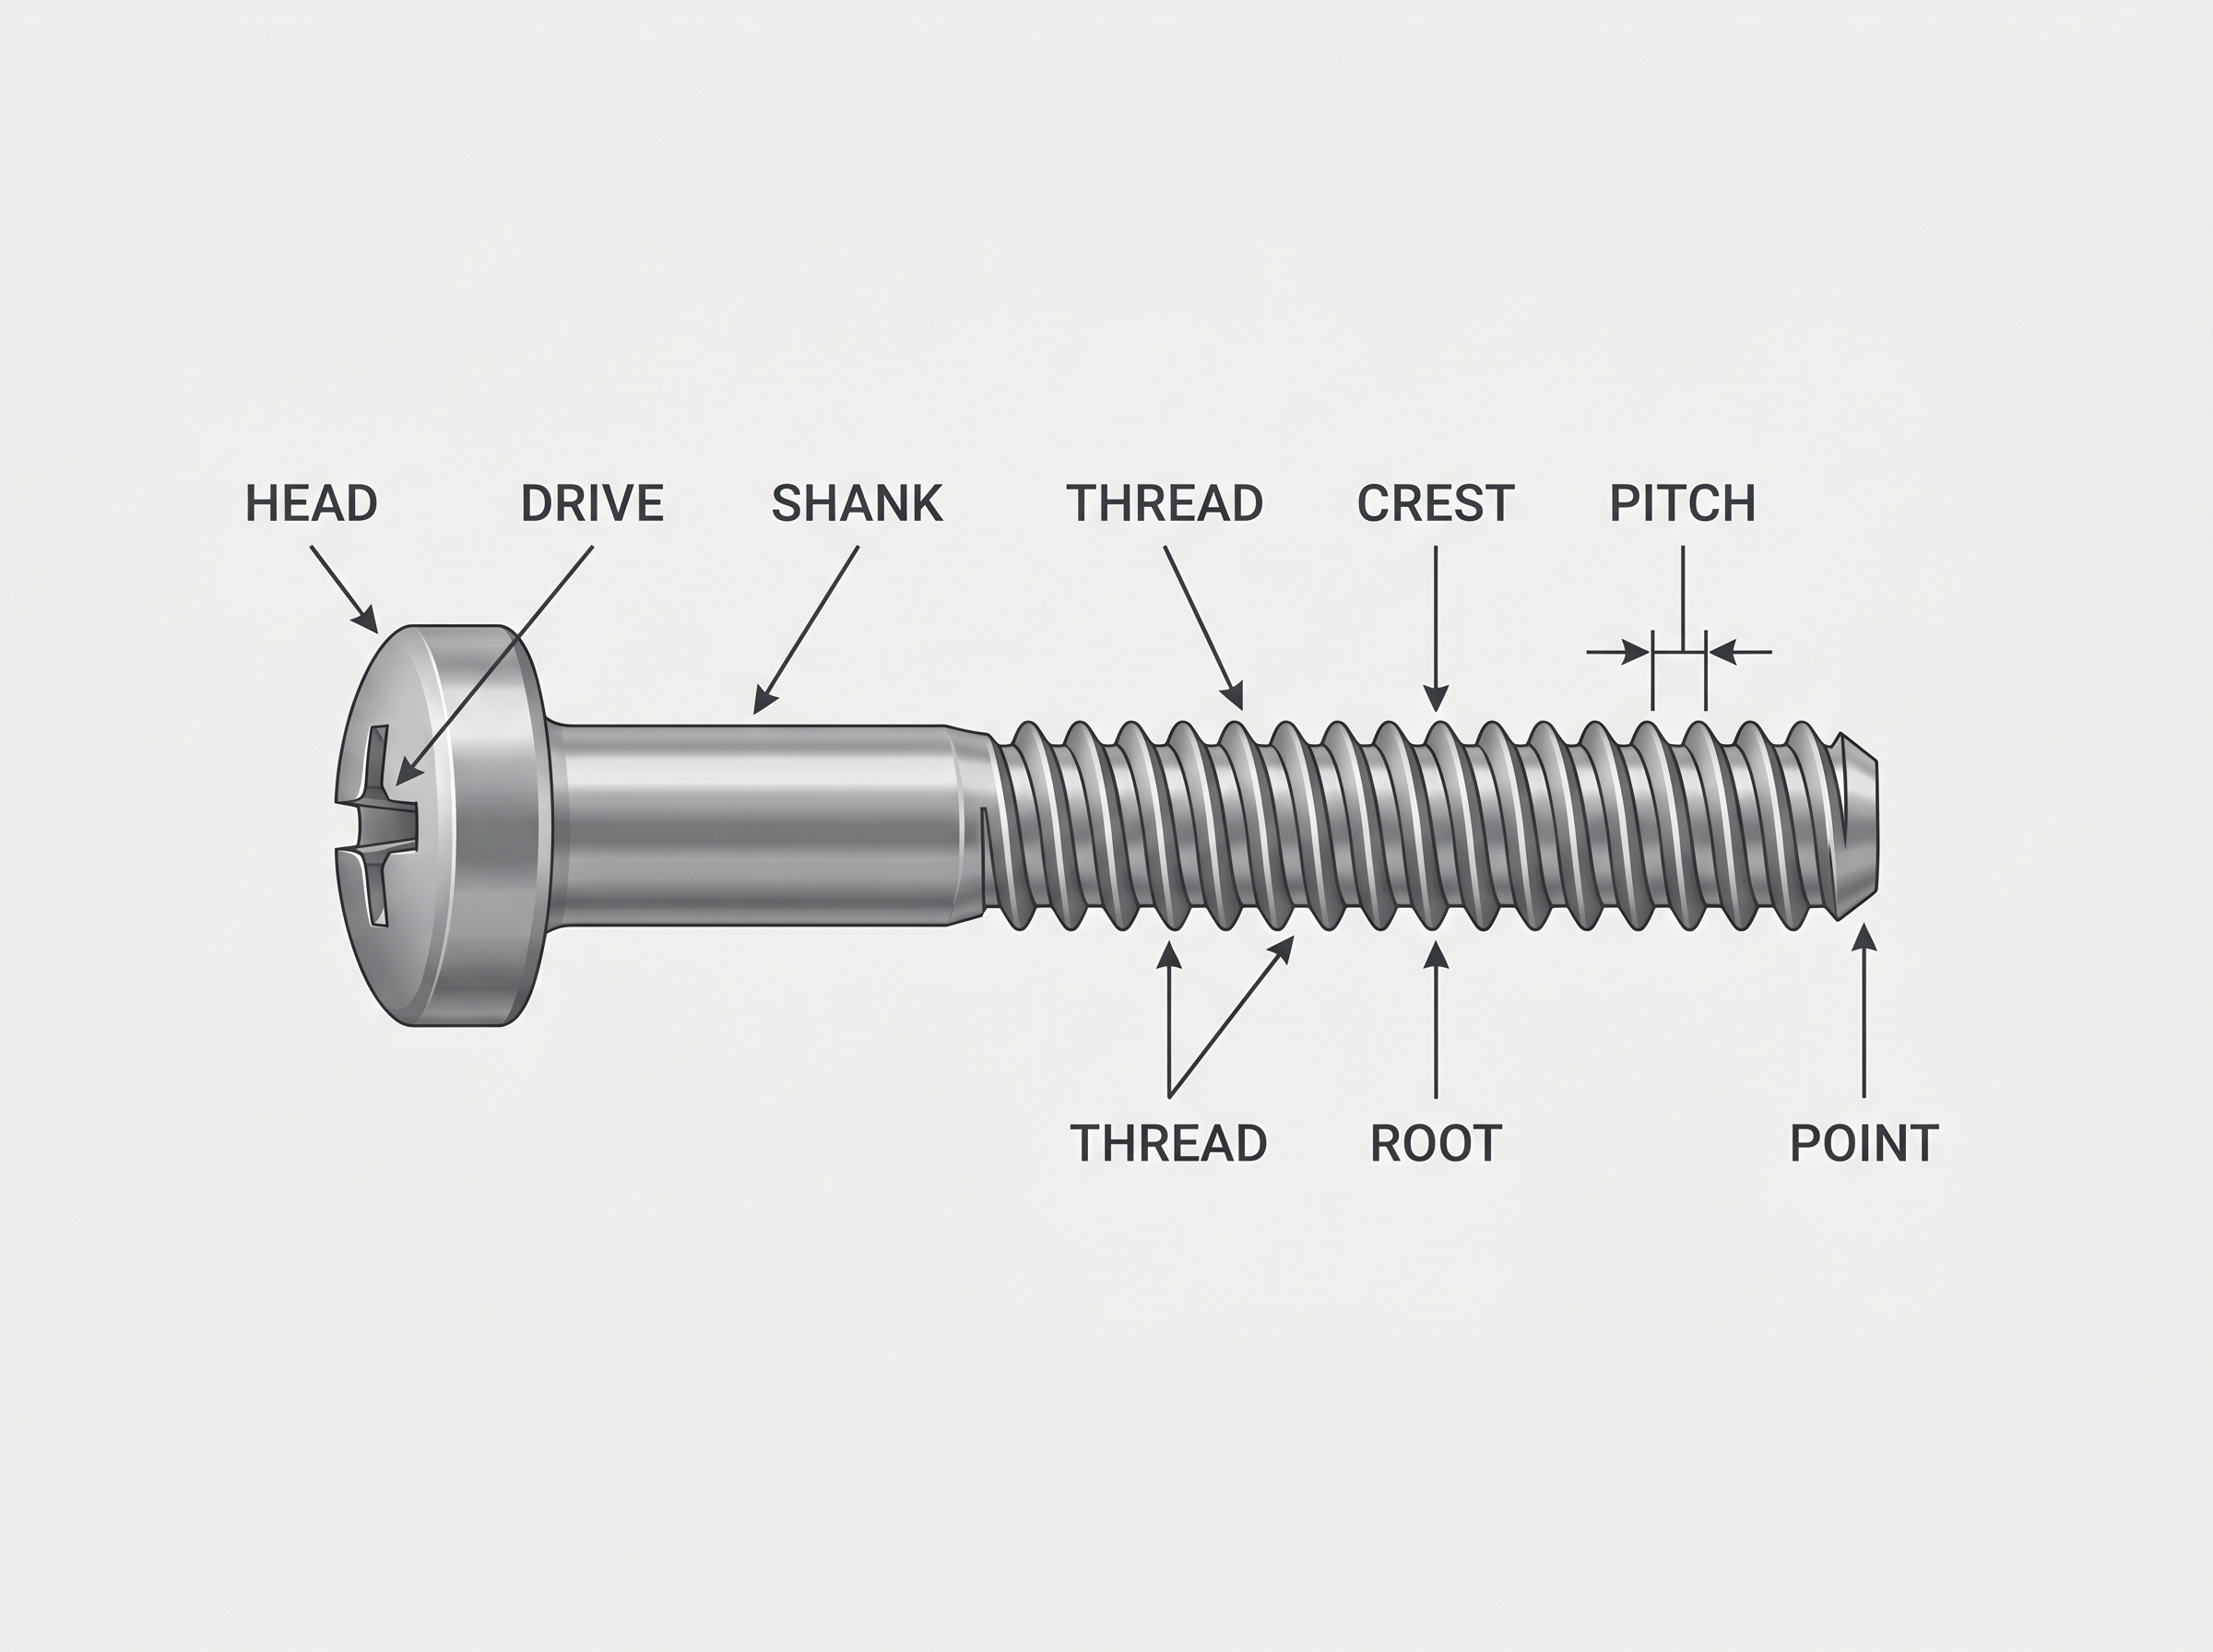
Effective thread engagement length refers to the length over which the screw threads actually enter and mechanically engage with the steel. Because light-gauge steel members generally have thin walls, the amount of material available to carry the thread load is limited. As a result, engagement length has a direct effect on connection strength.
If the screw only passes through the steel sheet without forming sufficient thread engagement, the connection may appear complete while providing relatively low pull-out resistance. Appropriate thread length increases the contact area between the screw and the steel and helps distribute the load more evenly.
Matching Thread Form to Light-Gauge Steel Thickness
Different thread forms and pitches are suited to different steel thicknesses and strength levels. A coarse pitch may reduce the number of effective engaged threads in thin steel, while a very fine pitch may increase installation resistance and reduce construction efficiency.
When evaluating thread engagement, steel thickness, screw diameter, thread depth, and the number of connected layers should be considered together. For thin-walled steel, the objective is not simply to use a longer screw. The objective is to ensure stable thread engagement while avoiding an excessive unengaged length after penetration.
Spinning, Thread Stripping, and Loosening Caused by Insufficient Thread Engagement
When thread engagement is insufficient, the screw may spin during installation. Spinning prevents the threads from continuing to cut into the steel and may damage the thread profile that has already been formed.
If the installer continues to apply torque, the connection may suffer thread stripping and lose its effective load-bearing capacity. Over time, vibration, temperature changes, and wind loads can further increase loosening. Therefore, thread engagement affects not only the initial installation but also the long-term stability of the light-gauge steel connection.
Pull-Out Performance and Main Failure Modes
Factors Affecting the Pull-Out Resistance of Self-Drilling Screws
Pull-out performance is an important indicator of light-gauge steel screw connection quality. The main factors affecting pull-out resistance include:
- Steel thickness and strength;
- Screw diameter;
- Effective thread engagement length;
- Screw head dimensions;
- Installation torque;
- Number of connected sheets;
- Contact condition between the screw and the steel.
In actual construction, pull-out resistance is not determined by a single screw parameter. It is the combined result of the screw, the steel substrate, and installation quality.
The Difference Between Pull-Out, Shear, and Screw-Head Pull-Over Performance
Pull-out resistance describes the ability of the screw to resist axial withdrawal from the connection surface. Shear resistance describes the ability of the screw to resist lateral movement and transverse loading. Screw-head pull-over is a different failure mode and commonly occurs when the sheet is too thin, the clamping force is excessive, or the washer and sheet are not properly matched.
In roof panels, wall panels, and light-gauge steel envelope systems, screws may be subjected to both tension and shear. Therefore, connection reliability should not be evaluated using pull-out data alone.
Common Failure Modes
Common connection failures in light-gauge steel structures include:
- Thread stripping: the local strength of the steel is insufficient and the threads are pulled out;
- Steel sheet tearing: the sheet tears around the screw;
- Screw tensile fracture: the screw itself cannot withstand the applied load;
- Screw-head pull-over: the screw head pulls through or causes local failure of the connected sheet.
These failure modes may occur individually or simultaneously when tension and shear act together.
The Effect of Installation on Connection Performance
Installation Angle and Drilling Process Control
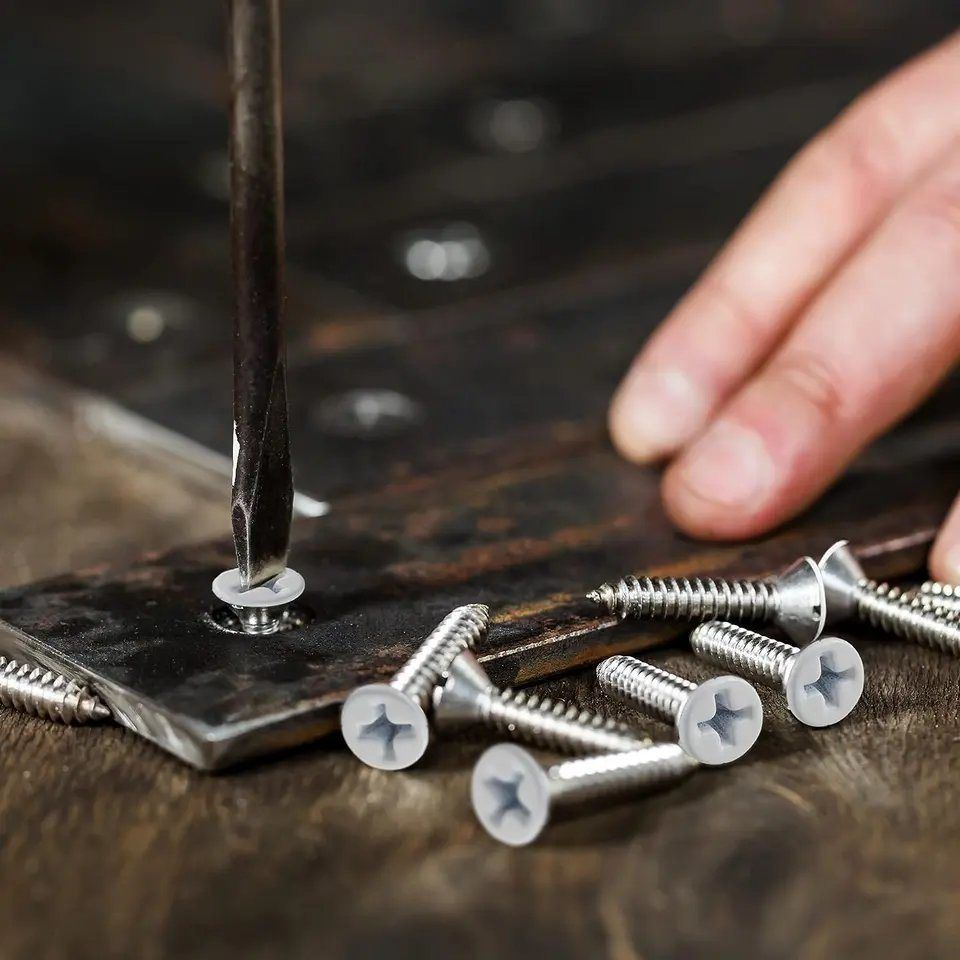
During installation, the screw should remain as perpendicular as possible to the connected sheets so that the drill point can cut evenly into the steel. Installation at an angle increases the risk of drill point wear and thread misalignment and may prevent the screw head from clamping the sheet evenly.
The installer should not forcefully increase torque before drilling is complete, as this may cause excessive heat in the drill point or local deformation of the steel.
The Effects of Excessive or Insufficient Torque
If torque is too low, the screw head may not clamp the connected sheet sufficiently, leading to sheet movement and local slippage. If torque is too high, it may damage the threads, pull the screw head through the sheet, or deform the screw head.
Therefore, installation torque should be matched to the screw diameter, steel thickness, sheet type, and installation tool. It should not be determined solely by operator experience.
Screw Spacing, Edge Distance, and Installation Consistency
If the screw is installed too close to the sheet edge, steel tearing may occur. If the spacing is too small, the stress zones around adjacent screws may overlap and reduce the efficiency of the overall connection.
For high-volume construction projects, screw spacing, edge distance, installation angle, and tightening level should remain consistent. Only when installation parameters are controlled can laboratory connection performance be more reliably achieved on site.
Basic Methods for Checking Connection Quality on Site
On-site inspection should focus on the following points:
- Whether the screw has fully penetrated the connected materials;
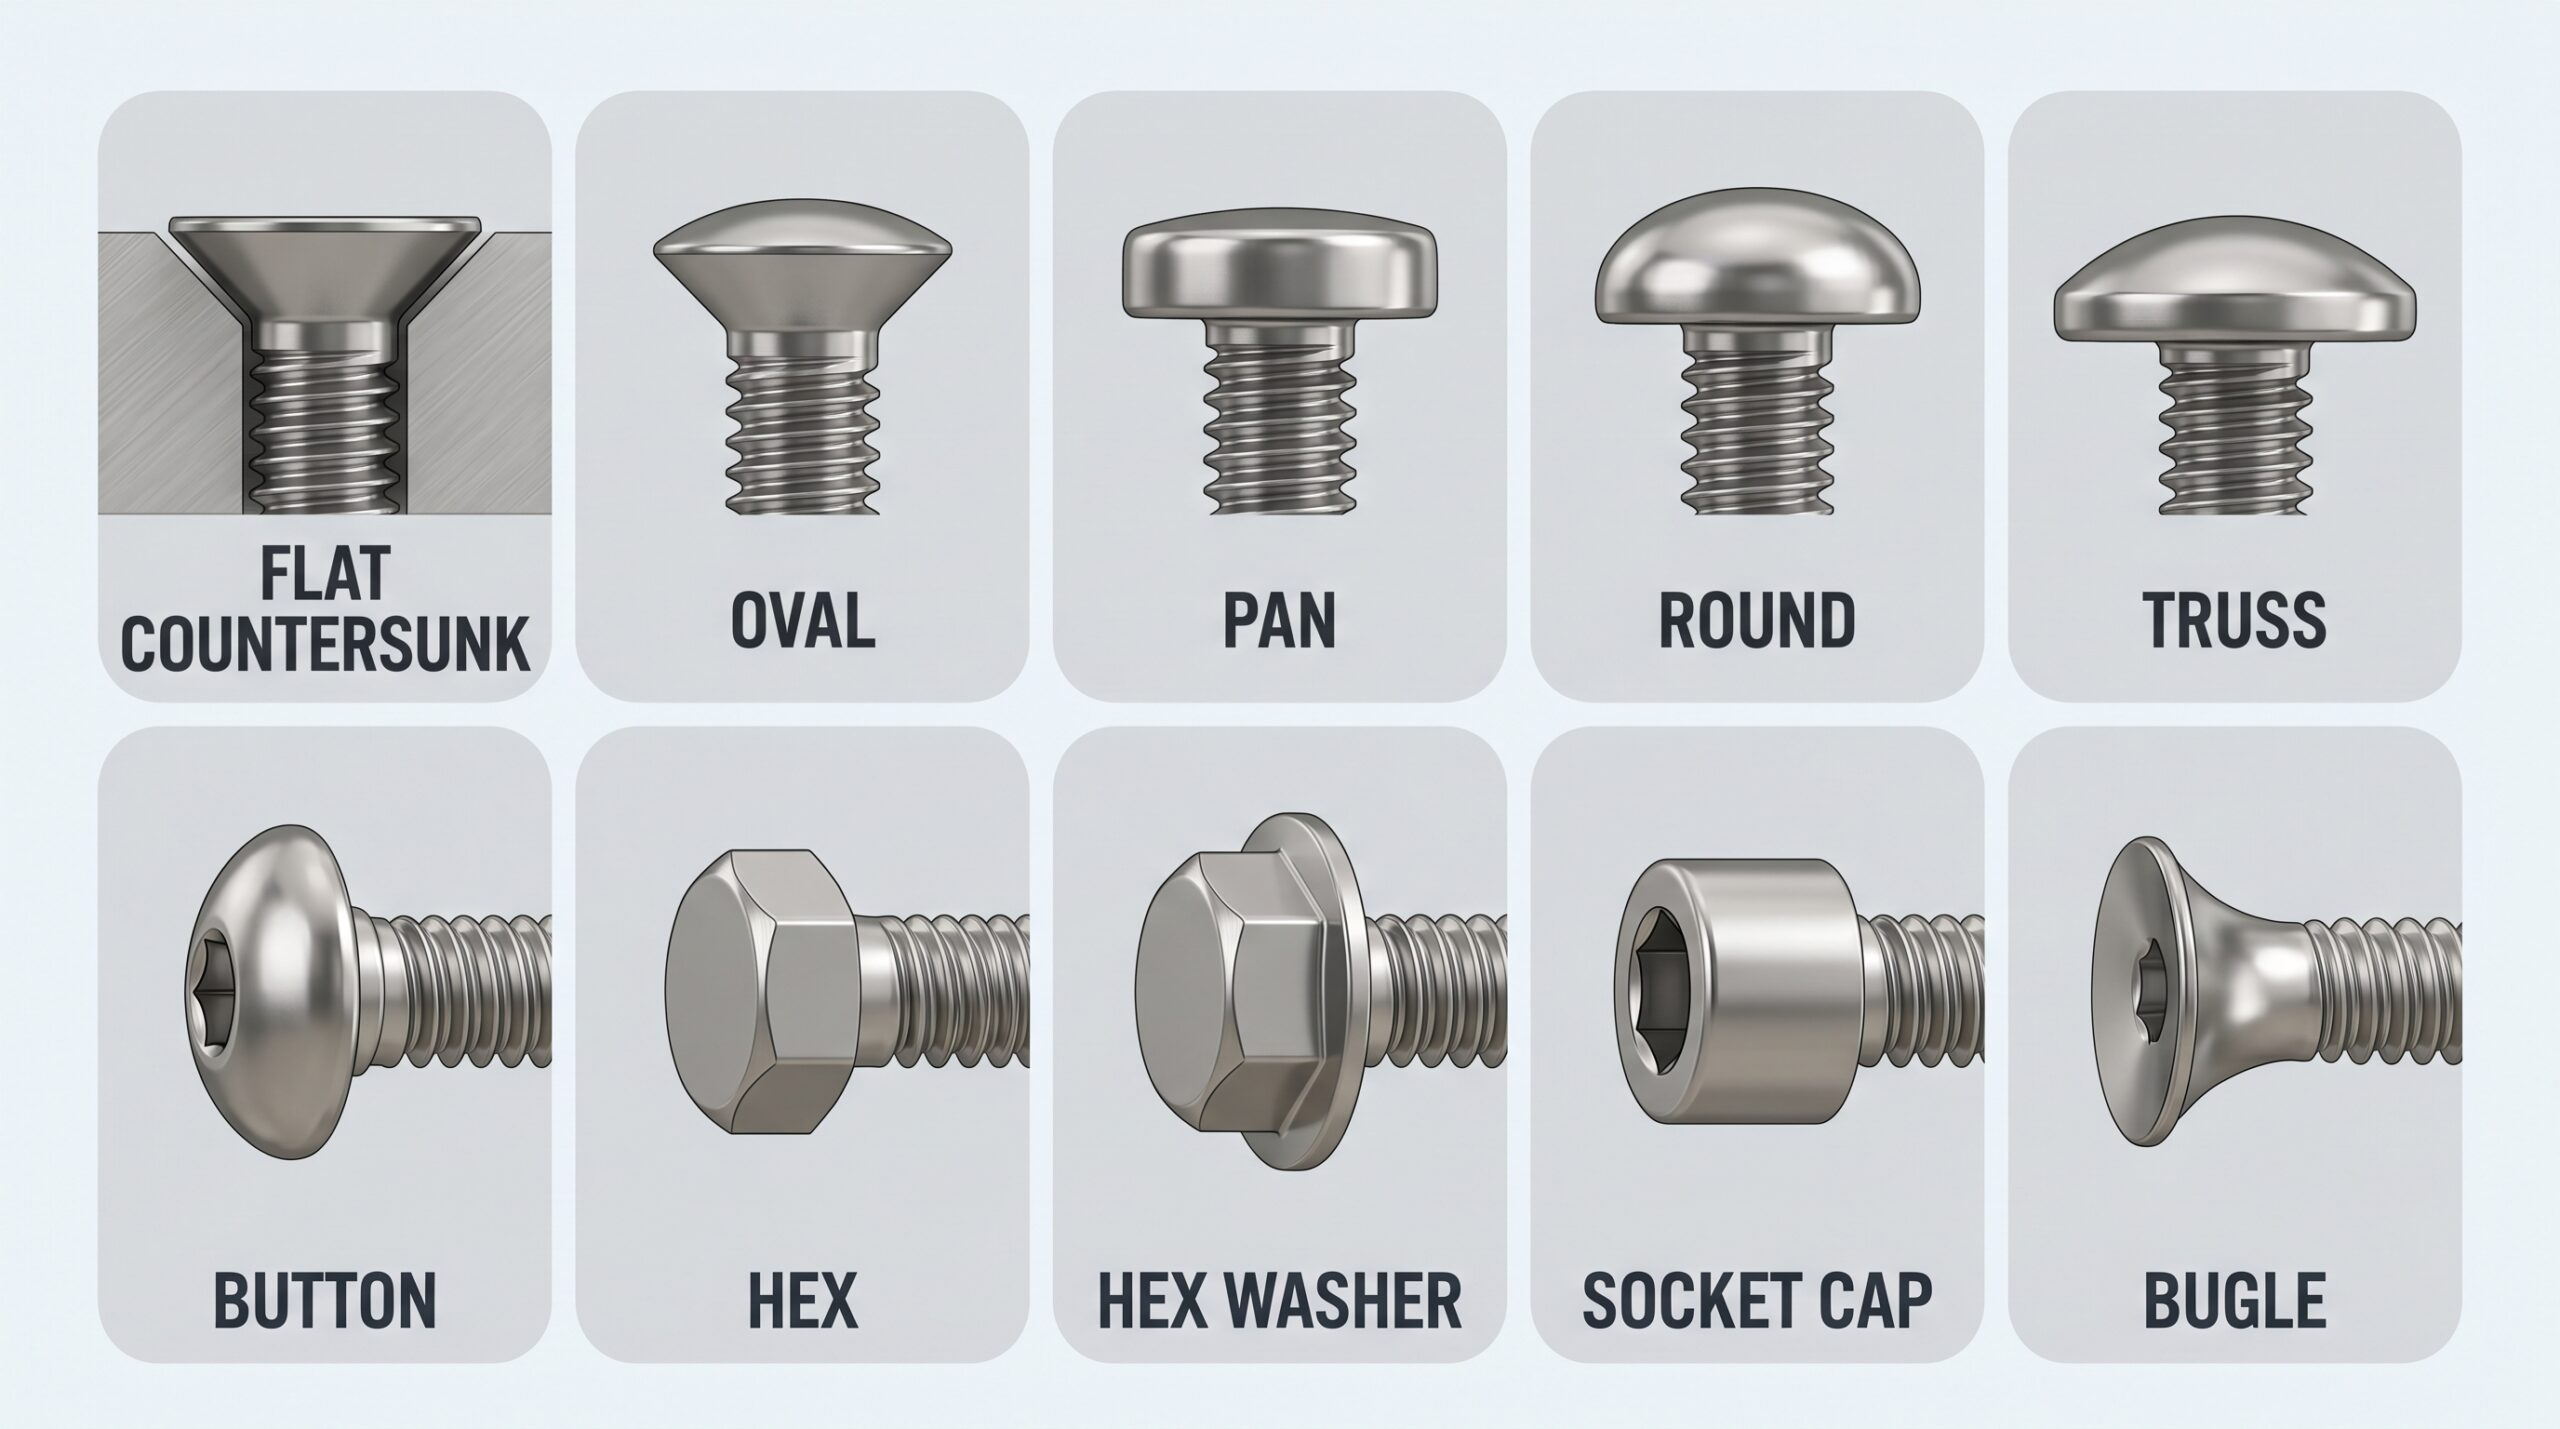
- Whether the screw head is flat and properly seated;
- Whether spinning, thread stripping, or angled installation has occurred;
- Whether cracks or visible deformation appear around the steel sheet;
- Whether screw spacing and edge distance meet construction requirements;
- Whether significant differences exist between individual connections in a production run.
Selection Methods for Different Light-Gauge Steel Applications
Connections Between Light-Gauge Studs and Wall Panels
Connections between light-gauge studs and wall panels generally require high installation speed, stable screw-head seating, and controlled surface compression. Screw length and thread form should be selected according to stud thickness, panel type, and the number of connected layers.
Connections Between Roof or Wall Panels and Light-Gauge Purlins
Connections involving roof panels and wall panels must satisfy pull-out and shear requirements while also addressing sealing, corrosion protection, and long-term wind loading. For exposed connections, the corrosion-protection system should be selected according to the environment, and the screw head and sealing area should be loaded evenly.
Structural Connections Between Light-Gauge Steel Members
Connections between light-gauge steel members generally carry higher loads than simple panel fastening. Particular attention should be paid to the total steel thickness, drill point capacity, thread engagement length, and the number of screws used.
For connection points that contribute directly to structural performance, selection should be based on engineering design, test data, and supplier technical documentation rather than appearance or general dimensions alone.
Selection Differences Between Indoor, Outdoor, and Highly Corrosive Environments
Indoor dry environments mainly require connection strength and installation efficiency. Outdoor environments also require consideration of moisture, temperature changes, and ultraviolet exposure. Coastal, industrial, and high-humidity environments require particular attention to corrosion resistance and long-term connection stability.
In these applications, material compatibility, surface treatment, washer sealing, and the electrochemical compatibility between the fastener and steel should all be included in the evaluation.
Engineering Procurement and Quality Evaluation
Core Parameters to Confirm During Procurement
When procuring structural self-drilling screws, the following parameters should be confirmed:
- Applicable steel thickness;
- Drill point type;
- Effective thread length;
- Pull-out and shear performance;
- Corrosion-protection grade.
It is also important to confirm the recommended installation tools, torque range, applicable connection materials, and batch inspection requirements.
Why Sample Testing and Batch Inspection Are Necessary
Screws with the same name or nominal dimensions may perform differently because of variations in material, heat treatment, drill point manufacturing, and surface treatment. For light-gauge steel projects, sample testing can verify actual drilling speed, thread formation, and pull-out resistance.
Batch inspection helps ensure that dimensions, hardness, and connection performance remain consistent between production batches, reducing quality variation during large-scale construction.
Why Fasteners Should Not Be Selected Solely by Price
Screw price reflects procurement cost, but it does not directly represent connection quality. Low-cost screws that suffer from drill point breakage, thread stripping, batch inconsistency, or corrosion failure may lead to rework, structural repairs, and project delays.
Therefore, engineering procurement should consider performance, application range, quality records, test documentation, delivery stability, and long-term service risk rather than comparing unit price alone.
Conclusion: Key Requirements for Reliable Light-Gauge Steel Screw Connections
The Drill Point Must Match the Steel Thickness
Drill point selection should be based on the total thickness, strength, and number of layers of the connected steel to ensure stable drilling.
The Threads Must Form Sufficient Effective Engagement
A reliable connection requires more than simply penetrating the steel. The screw must form sufficient effective thread engagement length to achieve stable load-bearing performance.
Pull-Out and Shear Performance Must Be Evaluated Together
Light-gauge steel connections are often exposed to complex loading. Pull-out resistance, shear resistance, and screw-head pull-over performance should therefore be evaluated together according to the application.
Correct Installation Is Essential for Achieving the Actual Connection Strength
Even when a screw has suitable technical performance, incorrect installation angle, torque, spacing, or edge distance can significantly reduce the actual connection strength. Only by combining correct selection, standardized installation, and quality verification can a reliable light-gauge steel screw connection be achieved.
Related News
Other news you might be interested in
Why Self-Drilling Screws Fail to Drill: A Substrate and Installation Checklist
When a self-drilling screw spins against steel without making progress, the purchasing decision becomes urgent: should the installer change the tool settings, should the buyer order a different screw, or should the supplier investigate the batch?A useful diagnosis starts by identifying exactly where drilling stops. Record the material at that point, check the selected screw against the assembly, and then compare installation conditions. This approach gives buyers a clearer basis for deciding what to change and what evidence to request.
Bulk Self-Drilling Screws: An RFQ Checklist for U.S. Importers and Distributors
When sourcing bulk self-drilling screws, a unit price is only useful if you know exactly what it covers. Two quotations may appear to describe the same product while differing in dimensions, coating, packaging, or delivery conditions. For U.S. importers and distributors managing several SKUs, those differences can make supplier comparisons difficult. A clear request for quotation—an RFQ—helps suppliers understand your requirements and gives your purchasing team a consistent basis for reviewing their offers. This checklist explains what to include, which details need confirmation, and how to turn an initial inquiry into a specification that both buyer and supplier can review.
Want to know more?
Get in touch with us for more information about our services and products.