
How to Securely Install Solar Panels on Metal Roofs While Preventing Roof Leaks
Han Congming
AuthorWith experience in screw and fastener manufacturing and sales, we operate our own production facility with stable large-scale capacity. We are specialists in self-drilling screws, drywall screws, chipboard screws, machine screws, bolts, and customized fasteners for construction and industrial applications.
The global solar PV industry is growing rapidly. In 2025, global solar PV additions reached a record 510 GW. Distributed solar is expected to account for 42% of total global PV capacity additions from 2025 to 2030. As more commercial and industrial buildings install rooftop solar systems, the role of industrial fasteners is no longer limited to holding components in place; they must also meet requirements for structural load-bearing capacity, environmental durability, and roof waterproofing. This is driving the industry away from selecting individual fasteners in isolation and toward more application-specific integrated fastening systems that consider connection strength, material durability, installation quality, and roof integrity together.
How Industrial Fasteners Perform Both Structural Connection and Roof-Sealing Functions
How Fasteners Connect PV Mounting Rails, Metal Roof Panels, and the Building Structure
In rooftop solar systems, fasteners may be used at the interfaces between modules and mounting rails, mounting rails and roof panels, or roof panels and the building substrate. Each connection must transfer loads to the next structural component and ultimately to the building structure. A failure at any point in this connection chain can affect the stability of the entire system.
Why Connection Load-Bearing and Waterproof Sealing Must Be Considered as a System
Exposed fasteners used on metal roofs not only provide structural connections but also work with the roof assembly to maintain a watertight seal. Washers, fasteners, roof panels, supporting substrates, and flashing details are interdependent. Replacing one component on its own does not automatically ensure that the entire detail will retain its original performance.
What Industry Requirements Do Fasteners Need to Meet in Rooftop Solar Applications?
These applications require consideration of mechanical strength, vibration resistance, corrosion resistance, compatibility with the roof assembly, and inspectability after installation. As a result, the fastener industry’s focus is expanding beyond individual dimensions and materials to include fastening-system performance and lifecycle quality management.
What Loads and Failure Risks Must Fasteners Withstand in Rooftop Solar Connections?
How Wind Uplift, Shear, and Pull-Out Forces Act on Screw Connections
When an array is exposed to wind, its connections may experience upward wind uplift, shear forces along the roof, and tension along the fastener axis. Actual loads depend on the project location, array layout, roof geometry, and connection design. The required connection performance cannot be determined from module weight alone.
How Roof-Panel Thickness, Substrate Material, and Connection Location Affect Load Capacity
Connection capacity depends not only on the fastener itself but also on roof-panel thickness, substrate material, effective thread engagement, fastener spacing, and connection location. The same screw may perform differently in substrates with different thicknesses or strengths, so the connection needs to be calculated or tested for the project conditions.
Why Fastener Strength Alone Is Not Enough
Even if the fastener itself does not break, the connection may fail if its threads pull out of the substrate, the roof panel tears locally, or the connection area deforms. Engineering assessments should identify the weakest part of the connected assembly rather than treating the screw’s tensile strength as the performance of the entire connection.
Understanding Pull-Out, Pull-Over, and Combined Loads in Connection Design
Pull-out strength describes a fastener’s resistance to being withdrawn from the substrate, while pull-over resistance concerns the risk of the fastener head or washer pulling through the panel. Actual connections may experience tension and shear at the same time, so the design method must apply to the specific materials, thicknesses, connection type, and governing code.
How Different Metal-Roof Configurations Affect Fastening Methods
Compatibility Requirements for Clamping Connections on Standing-Seam Roofs
On standing-seam roofs, clamp-based connections may reduce the need to penetrate the roof panel. Their suitability still depends on the panel profile, seam geometry, roof system, and design loads. Clamping systems must also account for thermal movement in the roof panels; the absence of roof penetrations does not eliminate the need for structural verification.
How to Handle Penetrating Connections on Corrugated and Exposed-Fastener Roofs
For corrugated panels and exposed-fastener metal roofs, the connection design typically needs to account for fastening location, substrate support, local panel performance, and waterproofing details at each penetration. Whether the fastener actually connects to the specified structural substrate cannot be determined simply by looking at the completed surface installation.
Matching Fasteners with Roof Panels, Mounting Rails, and Substrates
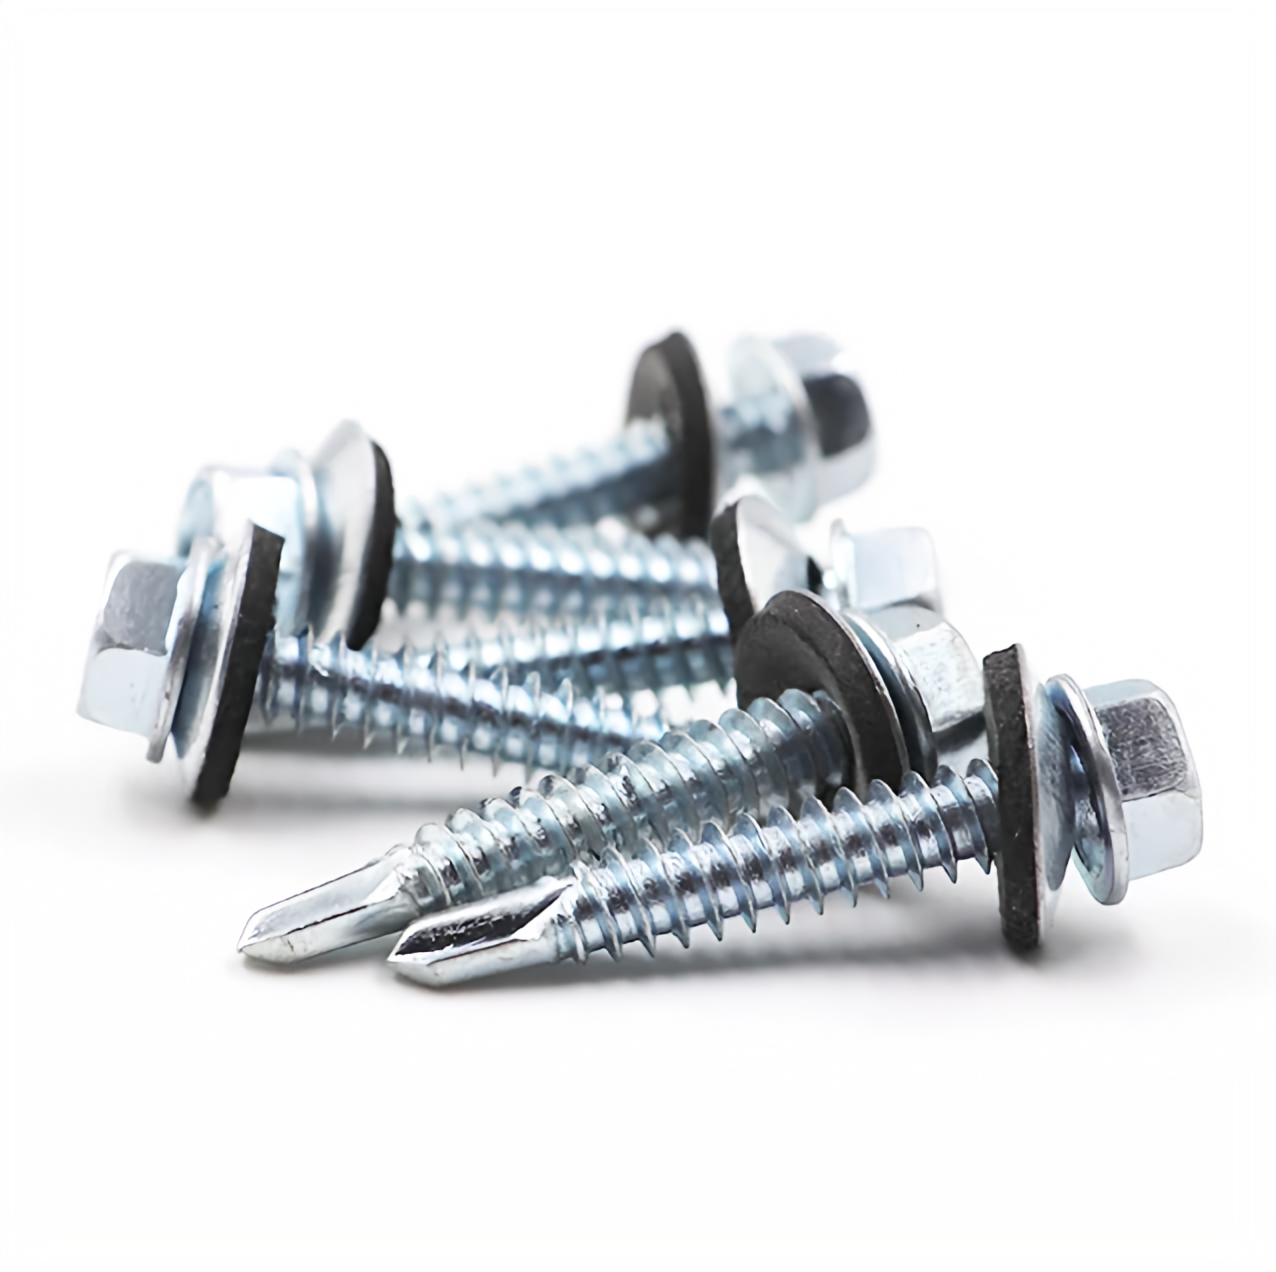
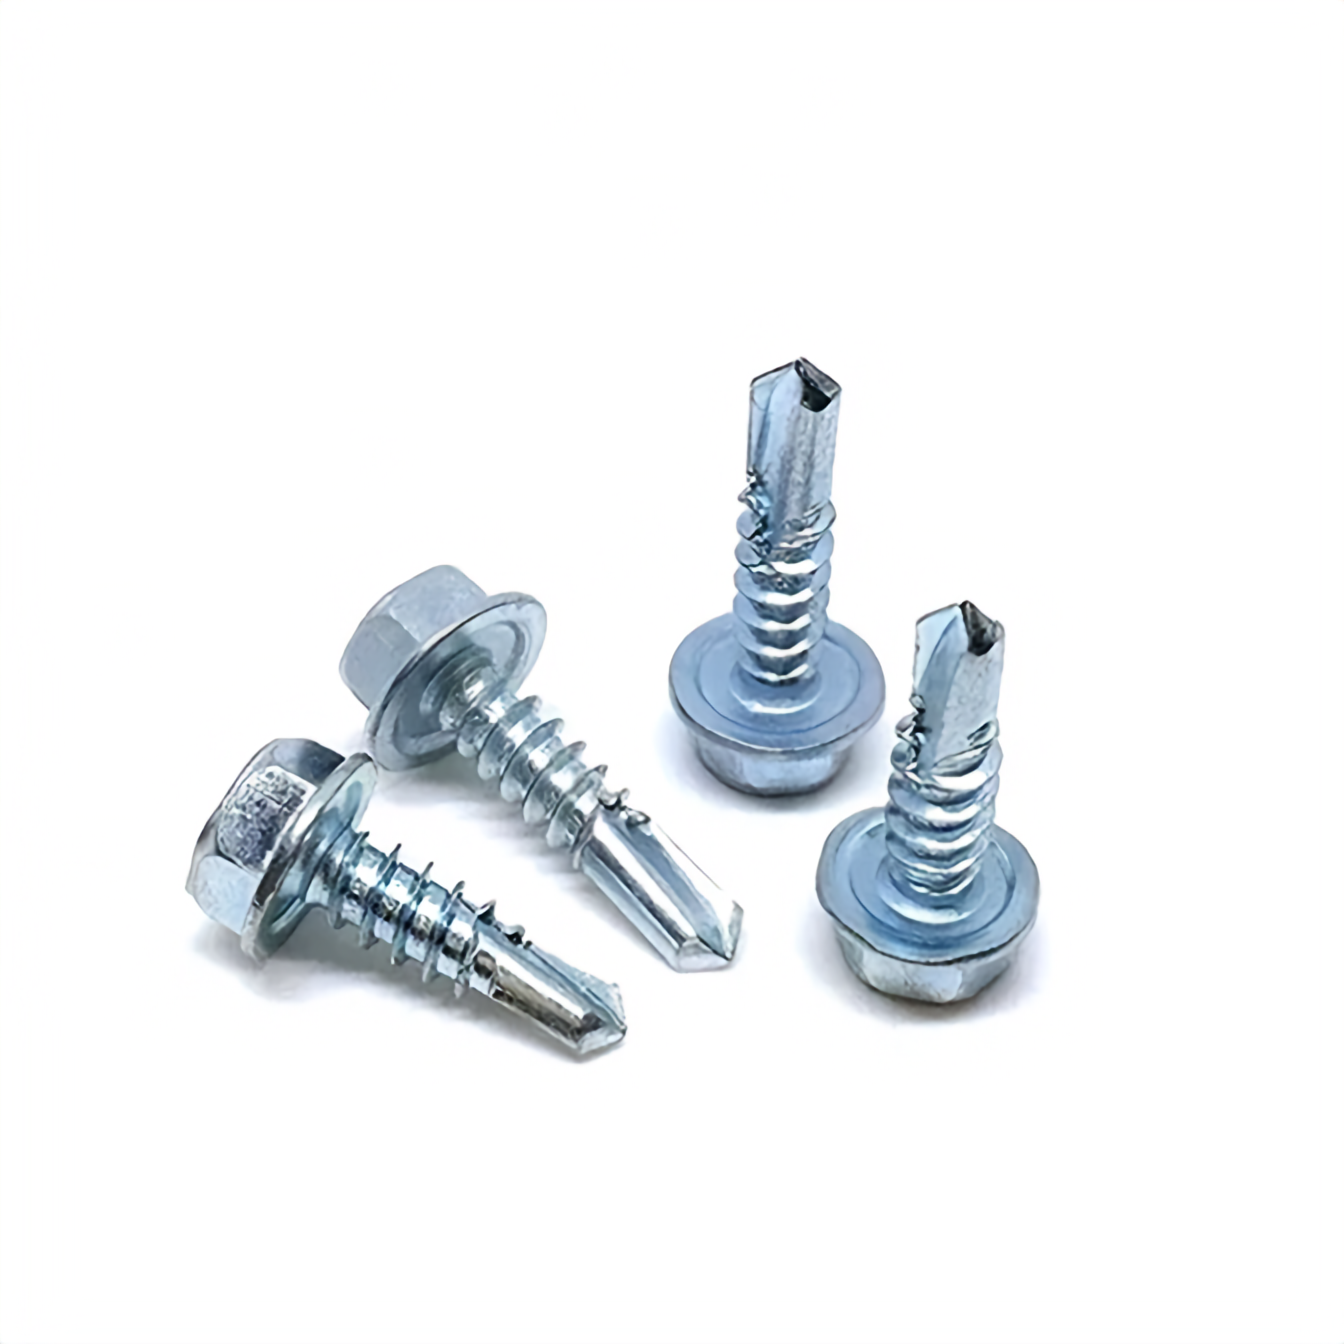
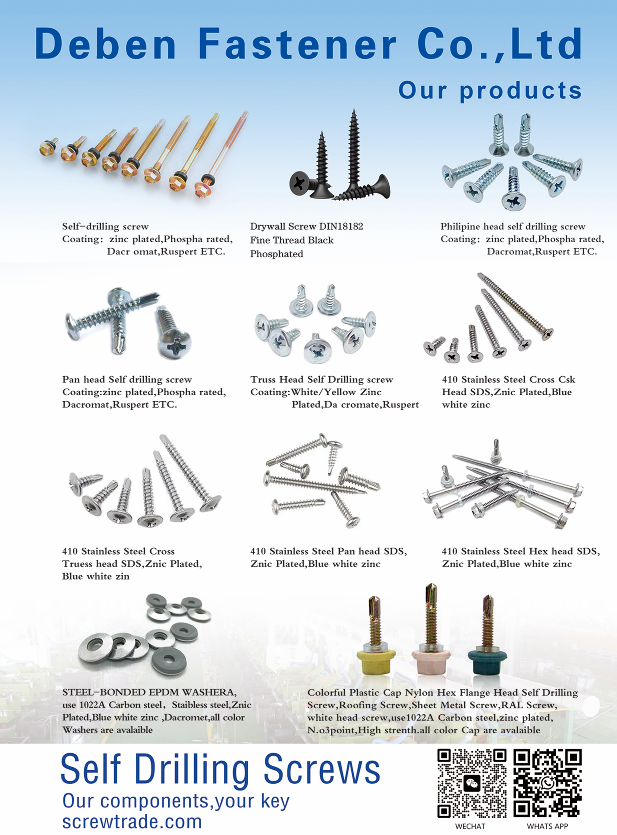
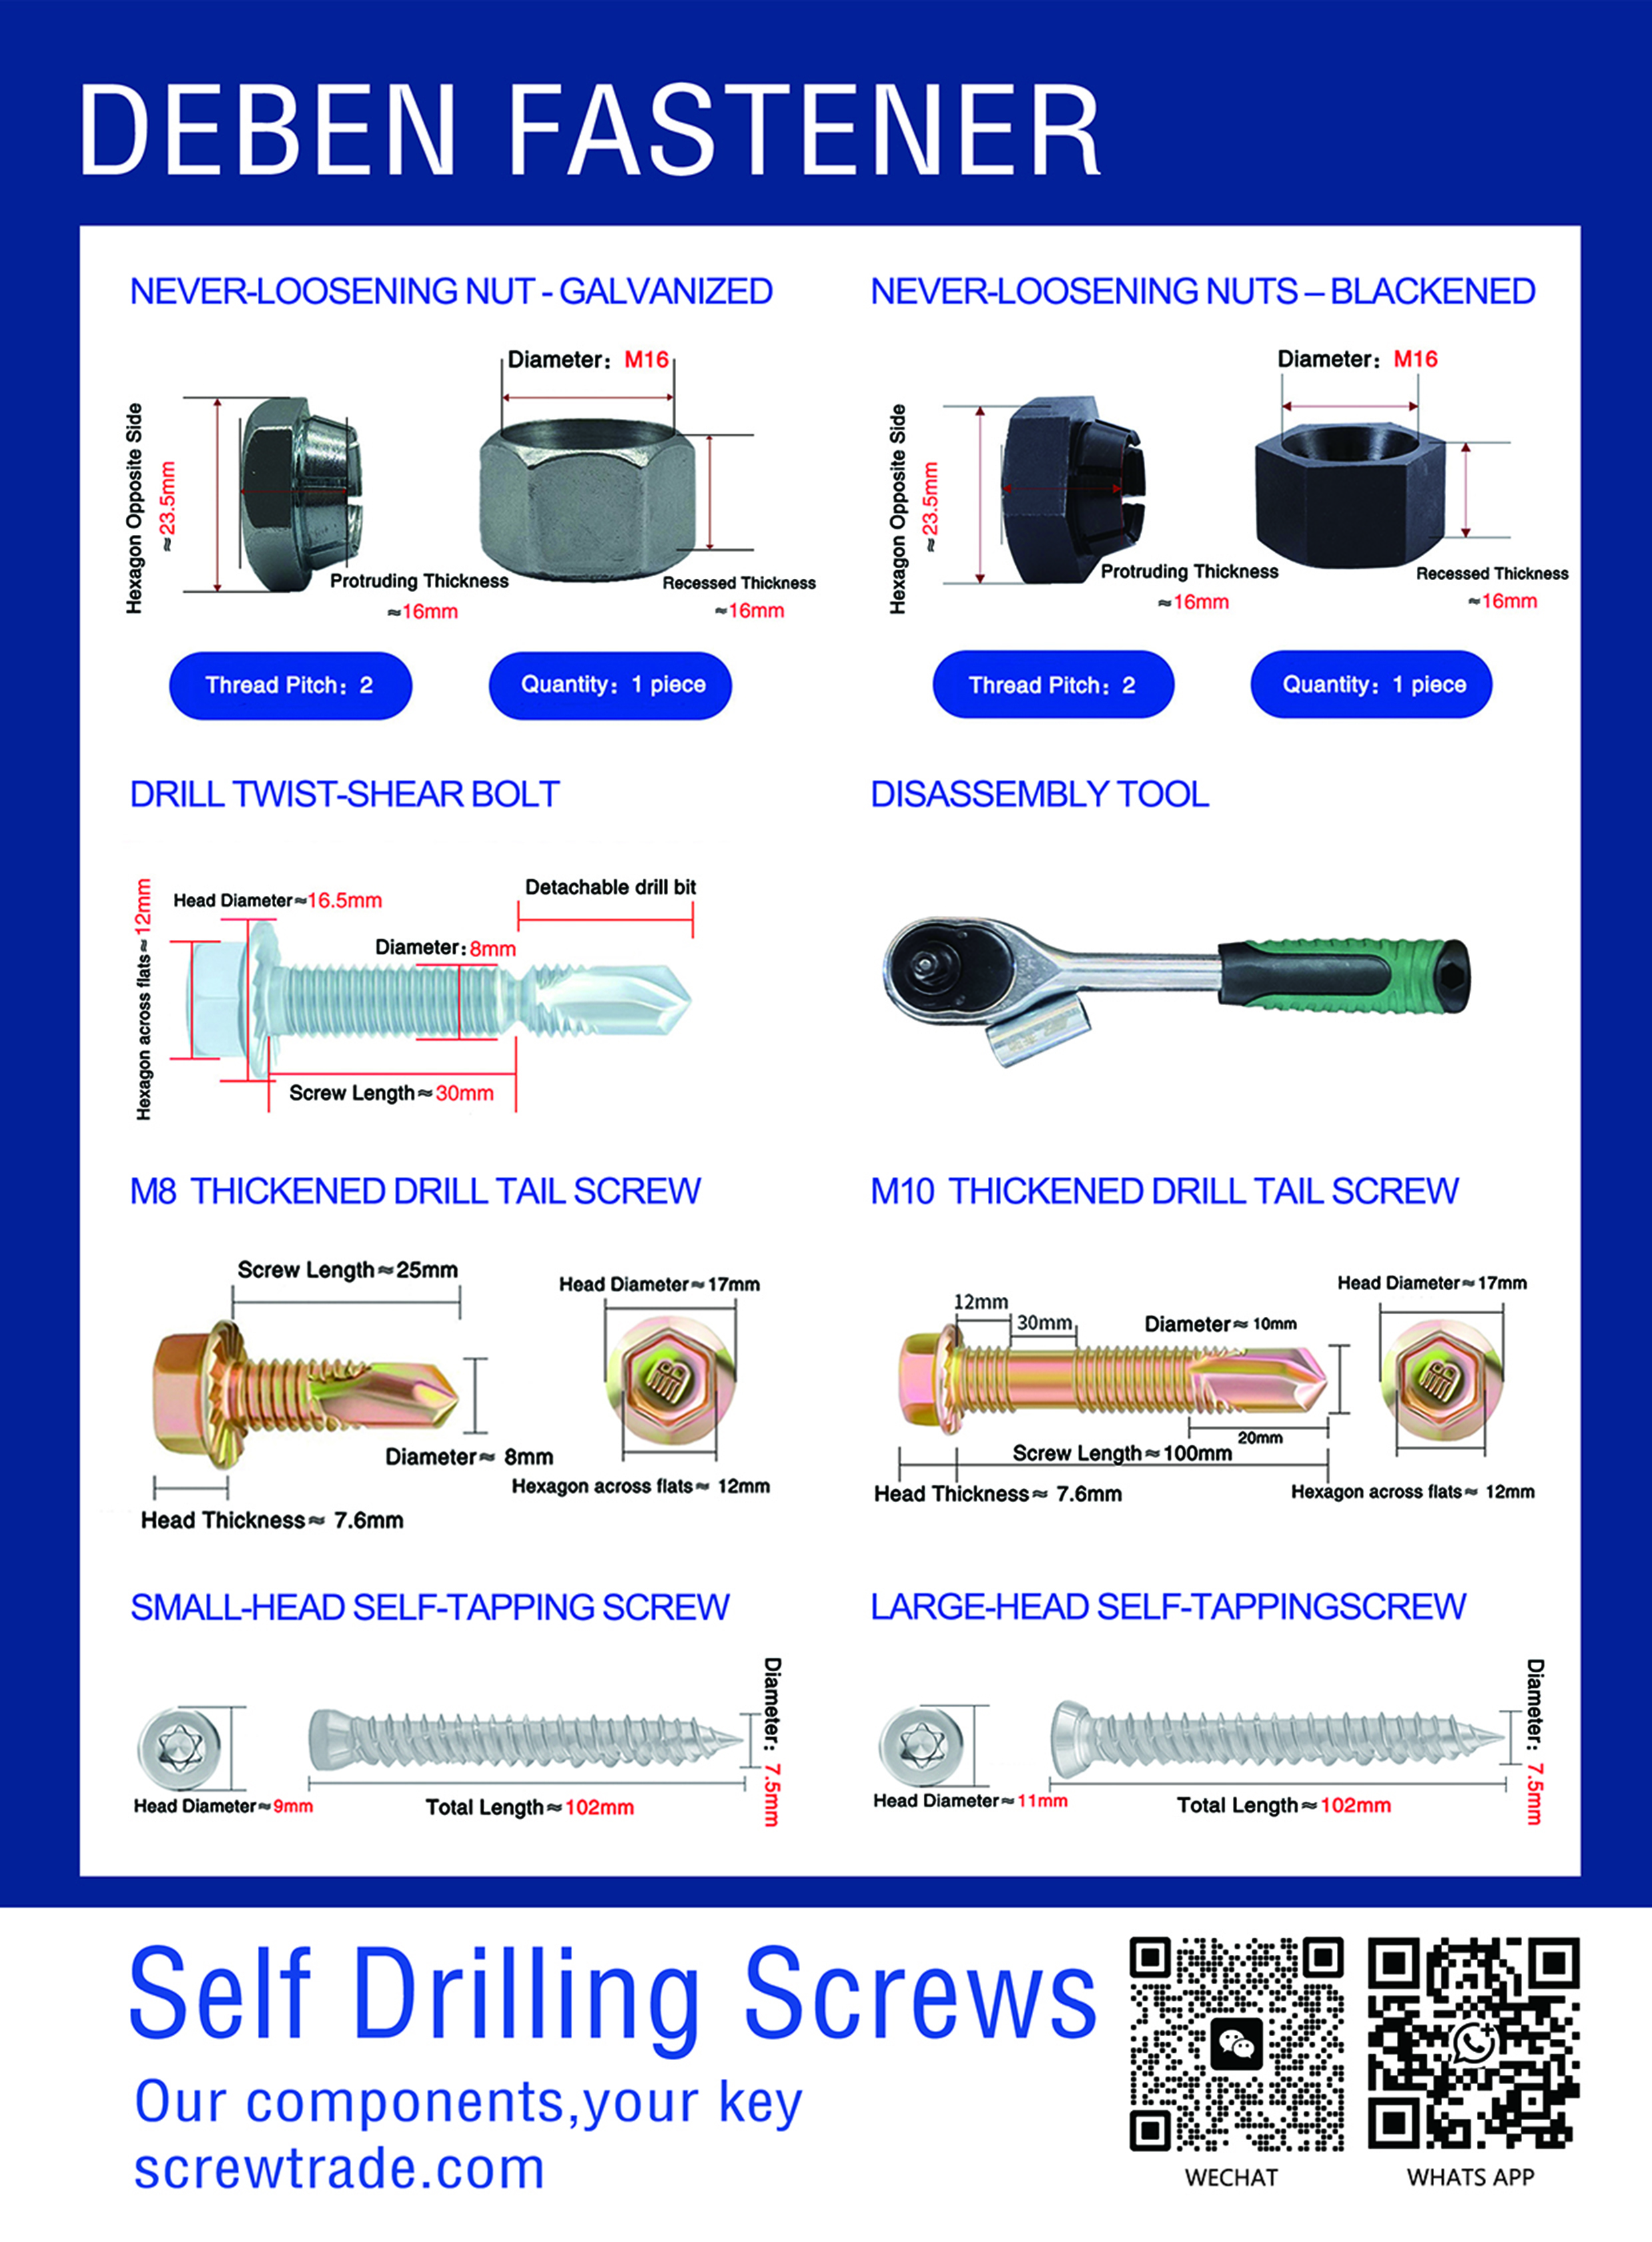
Metal roof fasteners must be compatible with the roof panels, mounting rails, substrate, and operating environment. The selection of exposed fasteners affects both connection strength and weather-tightness. Compatibility should be confirmed for the actual panel profile and material combination used in the project.
Why Unverified Components Should Not Be Substituted or Combined
Clamps, washers, screws, and mounting rails from different brands or models cannot be treated as equivalent simply because their dimensions appear similar. Unverified substitutions or combinations may alter connection geometry, load transfer, and sealing performance. Component combinations should be confirmed against evaluated system documentation and the relevant manufacturers’ instructions.
How Fastener Materials and Surface Treatments Affect Long-Term Roof-Connection Durability
Compatibility Among Fastener, Roof-Panel, and Mounting-Rail Materials
Where a connection includes different metals, their electrochemical compatibility should be assessed. When dissimilar metals are in contact in the presence of moisture or minerals, galvanic corrosion may occur and affect the long-term performance of fasteners, mounting rails, or electrical connections.
Corrosion Risks in Wet, Coastal, and Industrial Environments
Coastal salt spray, industrial pollutants, persistent moisture, and poor roof drainage may all increase corrosion risk. General material-selection practices should not be applied automatically to these environments. Both the exterior and interior building environments should be considered, and suitability should be confirmed against the guidance for the roof materials and fasteners.
What to Consider About Plating, Coatings, and Contact Between Dissimilar Metals
Surface treatments should be assessed in relation to the substrate, metals in contact, coating integrity, and environmental conditions. Scratches during installation or exposed substrate from field cutting or grinding may increase the risk of localized corrosion. Component selection should be based on a verified material combination.
How to Avoid Judging Durability by Coating Name Alone
A coating name such as “galvanized,” “stainless steel,” or a proprietary coating designation is not enough to determine the expected service life of a connection. Material grade, coating system, test conditions, contact materials, salt or pollutant exposure, and the relevance of test results to the specific roof system must also be verified.
Waterproofing Cannot Be Achieved by Fasteners Alone
How Screw Heads, Washers, Roof Panels, and Flashing Details Work Together to Seal the Roof
A sealing detail is formed by the fastener, washer, roof-panel surface, and flashing assembly together. A mismatch with the panel profile, incorrect installation location, or damage during construction can compromise the seal. The detail should therefore be evaluated as a complete system.
Why Fastener Installation Depth and Washer Compression Matter
A fastener that is too loose may not achieve the intended contact, while overtightening may deform the washer or affect the panel surface. For connections using EPDM sealing washers, the fastening condition should follow the applicable installation documentation. “Tighter means more waterproof” is not a substitute for proper installation.
How to Confirm Compatibility Between Sealants and the Roof System
Sealants should be compatible with the roof-panel coating and substrate, temperature changes, and exposure conditions. Their location and use should be defined by the roof detail. Applying sealant in the field should not be treated as a universal way to compensate for incorrect hole locations, improper fastening, or incompatible connections.
How to Distinguish Fastener-Seal Problems from Other Roof-Leak Causes
When a leak is found, distinguish between failure at a fastener penetration, problems with roof laps or flashing, blocked drainage, and condensation. The inspection should not be limited to the screw directly above the visible leak because water may travel along the panel or roof assembly before appearing inside.
How Installation Practices Affect Industrial Fastener Connection Performance
Process Control for Drilling, Thread Formation, and Effective Engagement
Self-drilling screws form a hole with their drill points before engaging the substrate with their threads. Whether thread engagement is sufficient depends on the compatibility between the fastener, panel thickness, substrate material, and installation conditions. Installation records should capture whether drilling, thread formation, and fastener seating were completed as intended.
Checking Installation Torque, Tool Settings, and Fastener Seating
Installation torque should follow the applicable system design documentation and manufacturer requirements. A universal torque value should not be provided without regard to the specific materials and connection conditions. Tool settings and operator consistency also affect fastener seating and washer compression, so critical connections should be included in field quality checks.
How to Identify Overtightening, Stripped Threads, Misalignment, and Drill-Point Failure
Common defects include tilted fasteners, stripped threads, visibly deformed washers, drill points that have not penetrated properly, or connections that become loose after installation. When a defect is found, investigate the substrate, fastener, tool, and installation process rather than trying to conceal the problem by tightening the fastener again.
How Installation Records and Field Inspections Improve Connection Consistency
Confirm fastener locations and connection details before installation, record deviations and corrective actions during construction, and retain inspection results at handover. These steps help improve the traceability of connection quality. Critical fastened connections should also be monitored for securement, vibration, and mounting-system deformation.
How Testing, Acceptance, and Traceability Can Verify Fastener-Connection Quality
What Connection Requirements Should Material and Dimensional Inspections Cover?
Quality inspections should verify that material, diameter, length, thread, head, washer, and surface treatment conform to the approved specifications. For rooftop solar connections, the delivered components should also match the design drawings and the evaluated system combination.
How to Validate Pull-Out, Shear, and Sealing Performance for the Specific Application
Pull-out performance, shear performance, pull-over resistance, and sealing should be evaluated for the relevant substrate, panel thickness, connection location, and load combination. In cold-formed steel connection design, shear, pull-over, pull-out, and combined loading are separate considerations. The scope and assumptions of a design method should not be extended beyond the project conditions for which it applies.
How to Link Product Batches, Test Records, and Installation Records
Procurement batches, material certificates, test reports, incoming inspections, and installation records should be traceable to one another. Lot traceability helps identify affected materials and installation areas if loosening, corrosion, or leakage occurs, rather than relying only on recollections from the site.
How to Check Certifications and Standards by Product, System, and Region
The scope, test conditions, system combination, and applicable region of a standard or certification should be verified. For example, in the United States, UL 2703 covers areas including PV mounting systems, clamping devices, and grounding components. Certification of an individual component should not be treated as proof that the entire roof connection has been structurally verified.
Common Fastener Failures in Rooftop Solar Projects and Their Industry Causes
Loose or Pulled-Out Connections: Check the Substrate, Loads, and Installation Process
Loose connections may result from vibration, connection slip, insufficient substrate engagement, installation deviations, or actual loads exceeding the design conditions. Inspections should cover the fastener, mounting rail, and connected panel, and distinguish between loosening and substrate pull-out.
Leakage: Check Penetration Locations, Sealing Details, and Roof Drainage
When a roof leak occurs, check penetration locations, washer condition, flashing details, panel-surface damage, and drainage paths. Replacing only the visibly affected fastener without identifying the water path and root cause may allow the problem to recur.
Corrosion: Check Material Compatibility, Environment, and Surface Treatment
Corrosion investigations should record the materials and coatings used for fasteners, mounting rails, and roof panels, and check for standing water, salts, pollutants, and coating damage. Corrosion at connections between dissimilar metals in a solar system may affect mechanical or electrical connections, so risk should not be judged by surface color alone.
Repeated Failures: Trace the Causes Through Design, Procurement, Installation, and Acceptance
Repeated connection problems require investigation across multiple stages: whether the design matches the loads and substrate, whether procurement changed any components, whether installation followed the required process, and whether acceptance checks covered critical connections. Failure analysis should address the entire system rather than only the damaged fastener.
Establishing a Fastener Quality Loop from Design Through Maintenance
Design Stage: Define Connection Conditions, Loads, and Roof Configuration
At the design stage, record the roof type, panel and substrate conditions, connection path, environmental exposure, and project loads, and identify the governing code system. The design should also identify critical connections and specify the calculations, tests, and field inspections required.
Procurement Stage: Verify Specifications, Materials, Test Documentation, and Scope
Procurement documents should define fastener specifications, materials, surface treatments, compatible components, and batch documentation requirements. Load or corrosion data supplied by a vendor should be used for engineering decisions only when the test method, materials, and conditions are relevant to the project.
Installation Stage: Install and Inspect According to Confirmed System Documentation
Installation teams should use confirmed component combinations and installation documentation, and record deviations, substitutions, and rework. Critical connections should be checked for fastening condition, structural connection, and sealing details. Fasteners and mounting rails should also continue to be inspected during system operation and maintenance.
Handover and Maintenance Stage: Retain Records and Periodically Inspect Connections and Seals
At handover, retain the design basis, material and test documentation, construction inspection records, and maintenance requirements. Inspection frequency should be determined by the project environment, system documentation, and local requirements. After severe weather or roof repairs, check for loose fasteners, corrosion, seal condition, and drainage.
Related News
Other news you might be interested in
Why Self-Drilling Screws Fail to Drill: A Substrate and Installation Checklist
When a self-drilling screw spins against steel without making progress, the purchasing decision becomes urgent: should the installer change the tool settings, should the buyer order a different screw, or should the supplier investigate the batch?A useful diagnosis starts by identifying exactly where drilling stops. Record the material at that point, check the selected screw against the assembly, and then compare installation conditions. This approach gives buyers a clearer basis for deciding what to change and what evidence to request.
Bulk Self-Drilling Screws: An RFQ Checklist for U.S. Importers and Distributors
When sourcing bulk self-drilling screws, a unit price is only useful if you know exactly what it covers. Two quotations may appear to describe the same product while differing in dimensions, coating, packaging, or delivery conditions. For U.S. importers and distributors managing several SKUs, those differences can make supplier comparisons difficult. A clear request for quotation—an RFQ—helps suppliers understand your requirements and gives your purchasing team a consistent basis for reviewing their offers. This checklist explains what to include, which details need confirmation, and how to turn an initial inquiry into a specification that both buyer and supplier can review.
Want to know more?
Get in touch with us for more information about our services and products.