
Thread-Forming Self-Tapping Screws vs. Thread-Cutting Screws: Choosing the Right Fastener for Sheet Metal Assemblies
Han Congming
AuthorWith experience in screw and fastener manufacturing and sales, we operate our own production facility with stable large-scale capacity. We are specialists in self-drilling screws, drywall screws, chipboard screws, machine screws, bolts, and customized fasteners for construction and industrial applications.
In modern sheet metal manufacturing, fasteners are no longer treated as simple connection components. The material, thickness, hole type, installation method, and service environment of the sheet metal all affect connection reliability. When a joint does not use a nut or a pre-tapped internal thread, thread-forming screws and thread-cutting screws represent two different fastening approaches.
Understanding how these two types of screws work helps manufacturers establish more reliable selection criteria for sheet metal fastening, equipment assembly, and automated production. Screwtrade’s industrial fastener product catalog includes self-drilling screws, roofing fasteners, washers, and other industrial connection components that can be used as references for different application requirements.
Why the Sheet Metal Industry Needs to Distinguish Between These Two Types of Threaded Screws
The Growing Need for Thin-Gauge, Lightweight and Nutless Connections
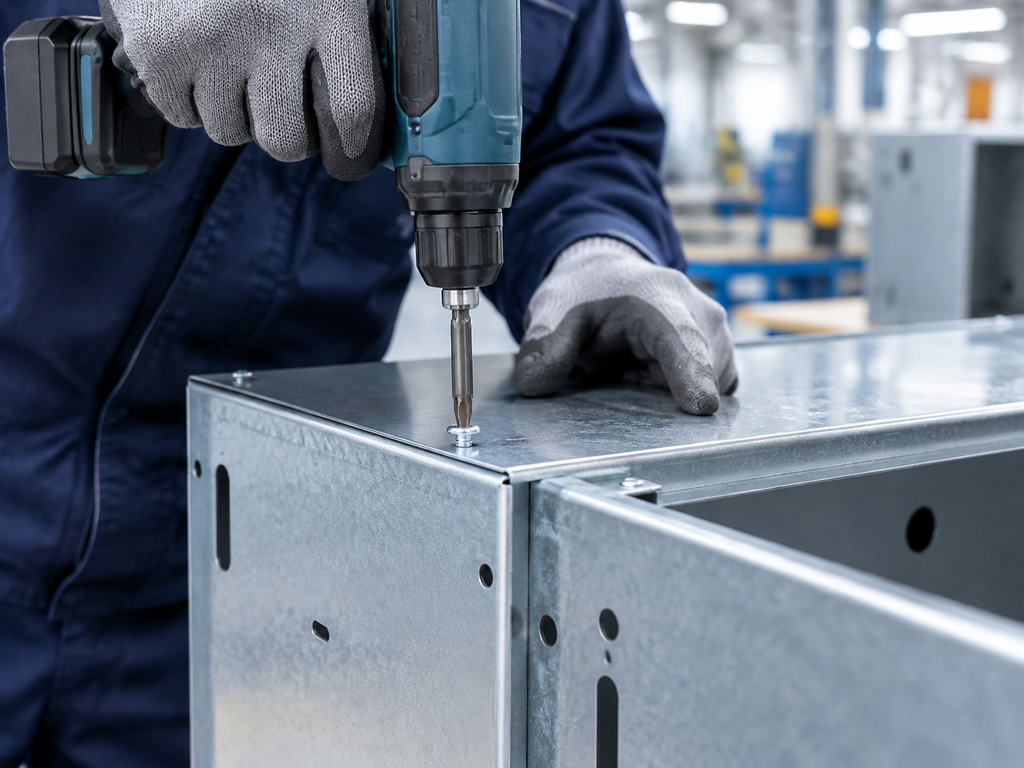
Automotive components, appliances, electronic equipment, and industrial enclosures increasingly use thinner and lighter metal sheets. Traditional bolt-and-nut connections often require additional space, processes, and components. As a result, self-tapping sheet metal screws can reduce assembly steps and improve production efficiency by creating a connection without a separate nut.
For applications that require drilling, thread formation, and fastening in a single operation, self-drilling screws can combine several processes. Their suitability still depends on the sheet thickness, drill-point capacity, and overall joint design.
How Thread Formation Affects Sheet Metal Connection Quality
When a screw enters sheet metal, it may form the thread by displacing material or by cutting material away. This directly affects hole-wall quality, thread engagement, pull-out resistance, and the risk of sheet deformation. Therefore, thread-forming screws and thread-cutting screws should not be interchanged based only on appearance or product name.
Screwtrade’s sheet metal screw types and material selection guide also treats substrate, total thickness, drill point, diameter, length, and thread engagement as part of an integrated selection process rather than evaluating diameter alone.
Balancing Production Efficiency, Joint Strength and Future Maintenance
High-volume manufacturing requires fast installation, while equipment maintenance requires adequate strength and disassembly capability. Engineering selection must therefore consider sheet metal assembly efficiency, service life, repair convenience, and chip control in the production environment.
For one-time assembly, installation speed may be the primary objective. For equipment enclosures, inspection panels, and industrial cabinets, however, repeat disassembly may be more important than initial installation speed.
How Thread-Forming Screws and Thread-Cutting Screws Work
Thread-Forming Screws: Creating Threads Through Plastic Deformation
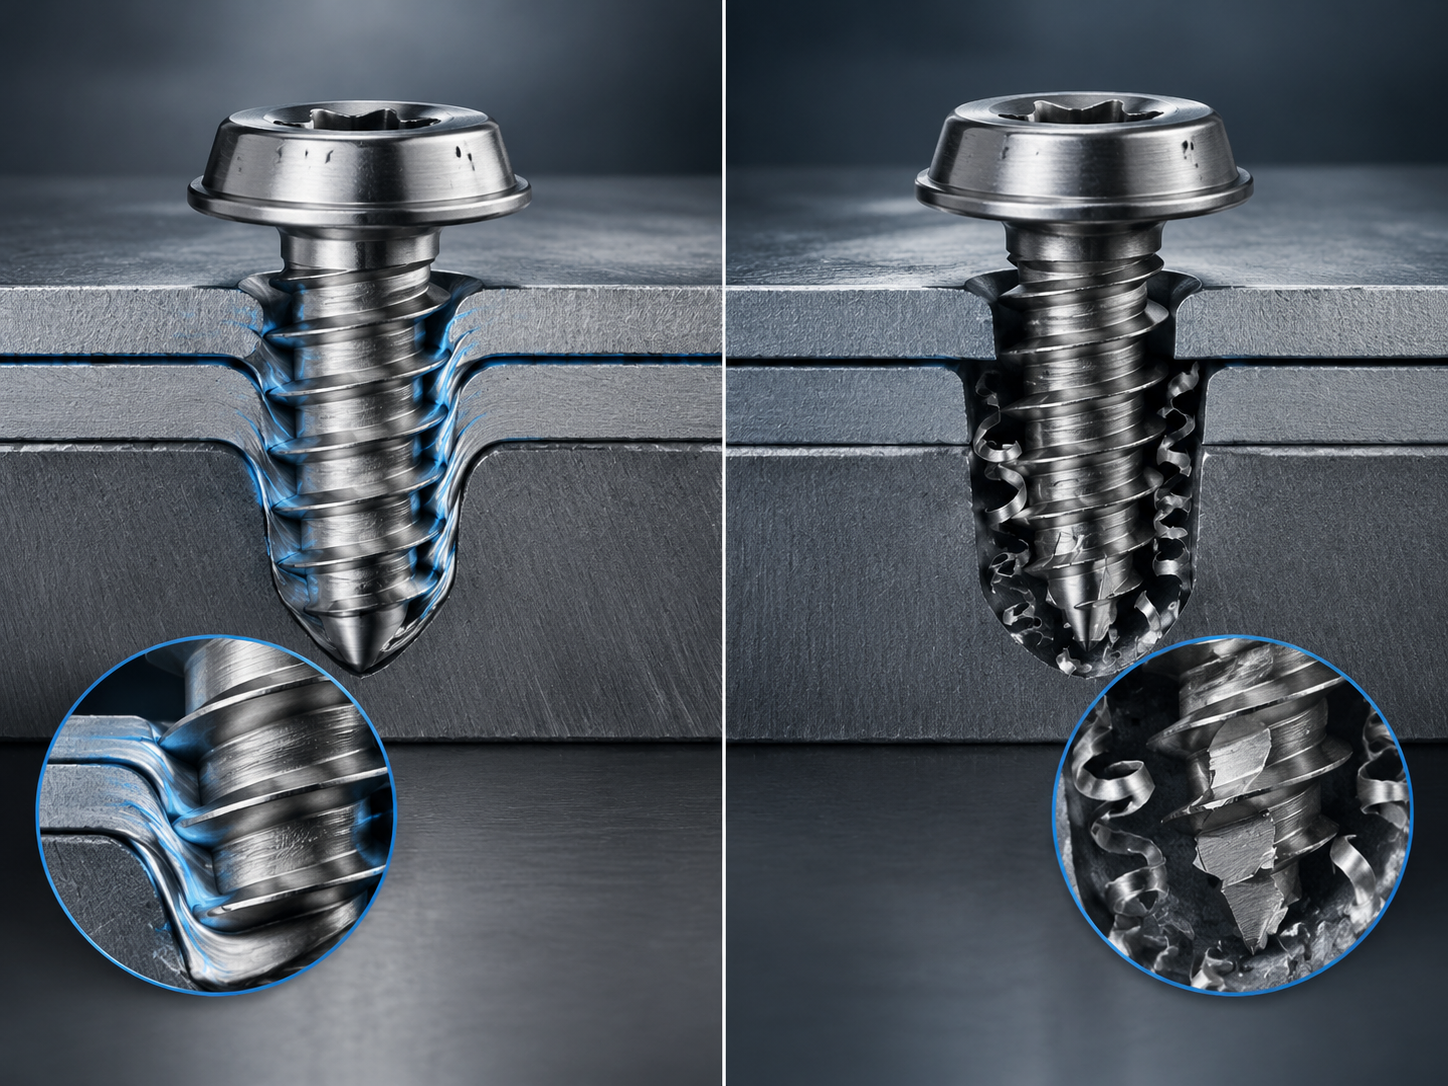
Thread-forming screws press against the sheet metal and cause the material to flow plastically along the thread profile. This creates an internal thread that matches the screw. Because relatively little material is removed, this fastening method generally preserves hole-wall continuity and produces limited chips.
For ductile thin steel sheet, aluminum alloy sheet, and certain softer materials, thread formation can reduce material loss. However, if the sheet is too thin or lacks sufficient ductility, excessive forming force may produce raised hole edges or local deformation.
Thread-Cutting Screws: Creating Threads by Cutting the Sheet Metal
Thread-cutting screws use cutting edges or cutting recesses to remove part of the material and create a thread inside the sheet. This method can be suitable for harder materials or specific pre-drilled holes, but chips, burrs, and hole-wall damage must be controlled.
The performance of a cutting screw depends not only on its thread profile, but also on the sharpness of the cutting edges, chip evacuation space, and condition of the installation tool. If chips cannot escape effectively, installation resistance may increase and the thread may not form completely.
The Relationship Between Self-Tapping Screws, Self-Drilling Screws and Sheet Metal Screws
Self-tapping screws are a broad industry category. They include screws that form threads through material displacement as well as screws that cut threads into the material. Self-drilling screws add a drilling function to the thread-forming process and may eliminate a separate pre-drilling operation, but their drill-point design and suitable sheet thickness must still be evaluated independently.
Screwtrade’s self-tapping versus self-drilling screw guide explains that conventional self-tapping screws generally require a pre-drilled hole, while self-drilling screws can perform drilling and fastening under suitable conditions.
The Fundamental Difference Between the Two Thread-Formation Methods
The basic difference is how the material is treated: thread-forming screws mainly displace material, while thread-cutting screws remove material to create the thread. This difference affects installation resistance, joint strength, chip generation, and repeat-assembly performance.
Engineering decisions should be based on sheet hardness, ductility, hole design, and service conditions rather than assuming that one type of screw is suitable for every sheet metal assembly.
Engineering Performance Comparison Between the Two Screw Types
Joint Strength and Effective Thread Engagement
Joint strength depends not only on screw material but also on effective thread engagement, sheet thickness, and thread integrity. In thin-sheet connections, insufficient engagement length may reduce the load-bearing area, while excessive forming force may deform the sheet.
During selection, engineers should confirm that the screw maintains sufficient effective thread engagement in the supporting material after passing through the outer sheet.
Pull-Out, Shear and Vibration Resistance
Pull-out resistance is primarily affected by sheet strength, thread engagement depth, and hole-wall condition. Strip-out resistance depends on whether the formed thread remains intact. In vibration environments, the clamping force between the screw and sheet, thread fit, and material fatigue behavior must be evaluated together.
For light-gauge steel components, equipment housings, and mechanical guards, it is also important to determine whether long-term vibration will enlarge the hole or loosen the screw.
Pre-Drilled Hole Requirements and Installation Resistance
Thread-forming solutions are generally sensitive to pre-drilled hole size. A hole that is too small increases installation resistance, while a hole that is too large reduces thread engagement. Thread-cutting solutions may tolerate certain hole conditions, but worn cutting edges or poor chip evacuation can also increase installation resistance.
In production, sample testing should be used to determine the relationship between hole size, installation speed, and sheet thickness.
Chip, Burr and Sheet Deformation Risks
Thread-cutting can generate metal chips. If these are not removed, they may affect electrical equipment, precision machinery, or moving components. Although thread-forming produces fewer chips, thin or insufficiently ductile sheet can still develop raised hole edges, cracks, or local deformation.
For this reason, chip management and sheet deformation control should both be included in the evaluation of sheet metal fastening processes.
Repeat Disassembly and Long-Term Maintenance
If a sheet metal assembly must be disassembled frequently, engineers should evaluate whether the thread can remain intact. Excessive material displacement may reduce repeat-assembly capability, while repeated cutting may enlarge the hole.
For serviceable equipment, repeated assembly testing should be used to monitor hole growth, thread wear, and clamping-force retention rather than judging performance from the first installation alone.
Selection Principles for Different Materials and Sheet Thicknesses
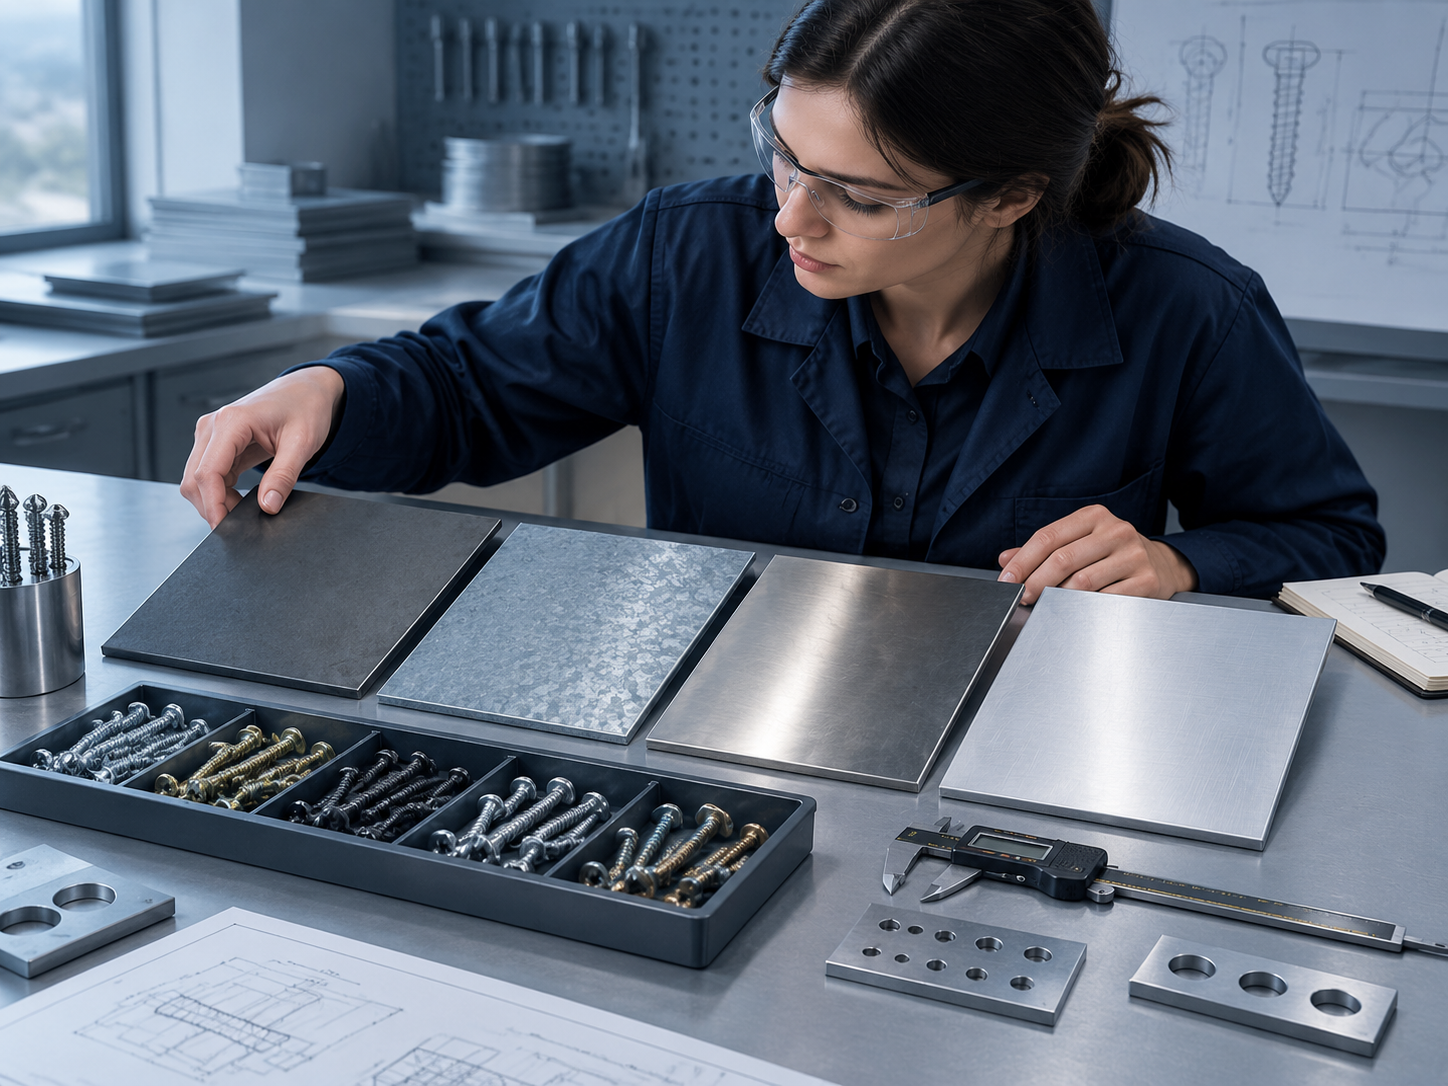
Differences Between Carbon Steel, Galvanized Steel, Stainless Steel and Aluminum Sheet
Carbon steel generally offers stable strength and machinability. Galvanized sheet requires careful control to avoid excessive damage to the protective coating. Stainless steel is harder and more sensitive to cutting capability and installation resistance. Aluminum alloy is relatively ductile, but thread wear and resistance to stripping require special attention.
For corrosive environments, engineers may refer to Screwtrade’s bi-metal self-drilling screw product page and 304 stainless steel self-drilling screw product page, while still validating the final material choice against the actual sheet and service environment.
Selection Requirements for Thin, Medium-Gauge and Multi-Layer Sheet
Thin sheet is more likely to experience hole-edge deformation and thread stripping. Medium-gauge sheet places greater emphasis on drilling capacity, effective thread engagement, and connection stability. For multi-layer assemblies, screw length should be determined according to the total joint thickness so that the thread does not remain only in the outermost layer.
The Effect of Material Hardness and Ductility on Thread Formation
Sheet with good ductility may be suitable for a thread-forming solution, while harder or less plastic materials may require stronger cutting capability.
When material hardness and ductility are not matched to the screw design, installation difficulty, screw breakage, hole-wall damage, or insufficient thread load capacity may occur.
Differences Between Pre-Drilled, Pre-Punched and Unperforated Applications
Pre-drilling improves hole-position accuracy, while pre-punching is suitable for high-volume stamping operations. Unperforated sheet relies on self-drilling screws to perform both drilling and fastening.
Different hole types change installation resistance, thread-formation quality, and production cycle time. The same installation parameters should not be applied automatically to every hole condition.
Determining Thread Engagement Length According to Sheet Thickness
Screw length should cover the effective joint layers while maintaining sufficient thread engagement. If the screw is too short, joint strength may be insufficient. If it is too long, it may penetrate the back of the assembly, interfere with internal components, or increase corrosion risk.
In multi-layer assemblies, engineers should also account for washers, brackets, insulation, and spacers that reduce the effective thread-engagement length.
Applications of the Two Screw Types in Manufacturing Industries
Automotive and Metal Component Manufacturing
Automotive components typically require lightweight construction, vibration resistance, and high-volume assembly efficiency. For body panels and bracket assemblies, engineers must balance joint strength, production cycle time, and future service requirements.
In these applications, the thread design must be compatible with stamping processes, automatic screw feeding, and electric-tool parameters.
Appliances, Electronic Equipment and Electrical Enclosures
Appliance and electronic equipment housings often use thin steel sheet, galvanized sheet, or aluminum alloy. In addition to mechanical strength, the fastening method must control visible deformation, metal chips, and electrical safety risks.
If the equipment requires regular service access, repeat disassembly capability and hole stability should also be considered during design.
Machinery Housings and Industrial Cabinets
Industrial cabinets commonly require repeated disassembly and long-term operation. Key concerns include thread durability, vibration resistance, and the ability to replace or reinstall fasteners during maintenance.
For these assemblies, maximizing initial installation speed alone may not produce the best engineering solution. The screw’s effect on internal components, cables, and protective structures should also be considered.
Construction Metal Components and Light-Gauge Steel Structures
Construction metal components place greater emphasis on sheet thickness, environmental corrosion, connection stability, and installation efficiency. Different structural locations may require different sheet metal screw types, selected according to load direction and service environment.
For roofing, wall panels, and steel-frame connections, engineers can refer to Screwtrade’s metal roofing self-drilling screw guide. However, the focus of this article remains the thread-formation mechanism rather than a specific roofing product recommendation.
Sheet Metal Components Requiring Automated High-Volume Assembly
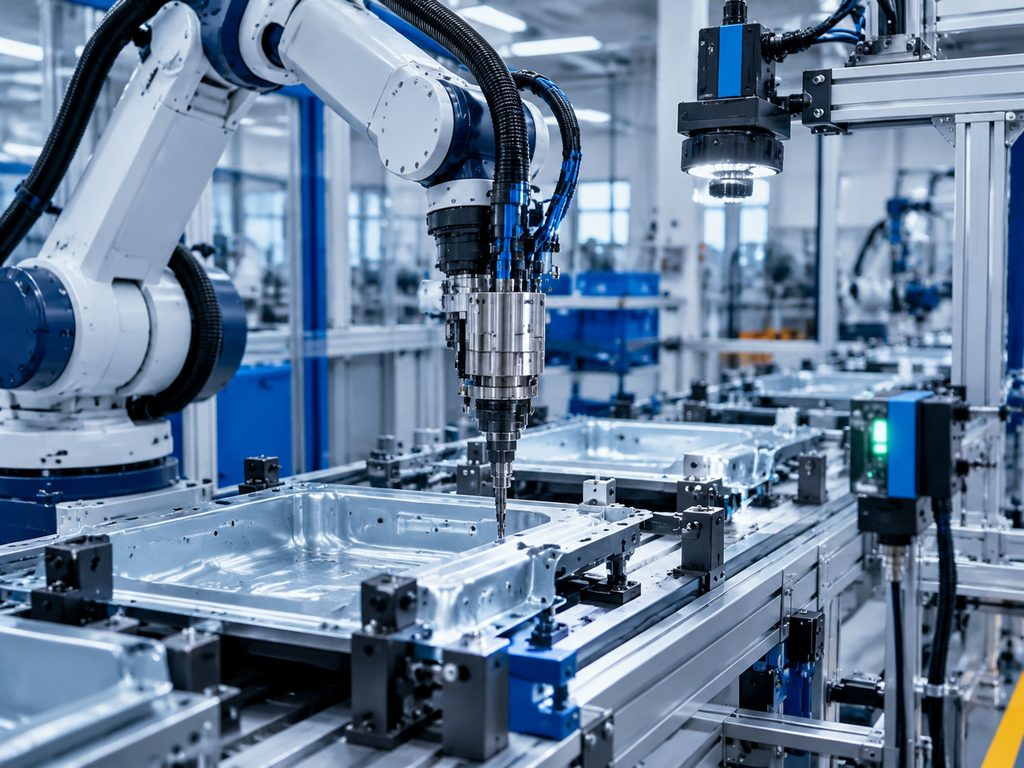
Automated production lines require stable screw feeding, dimensional consistency, and predictable installation resistance. The development of metal fastening technology is also bringing fasteners into closer integration with electric tools, vision inspection, and process-monitoring systems.
In high-volume assembly, consistency across production batches is more important than the short-term performance of a single sample.
Common Connection Failures and Quality-Control Methods
Thread Stripping, Hole Enlargement and Insufficient Clamping Force
Thread stripping is commonly related to excessively thin sheet, oversized holes, insufficient installation resistance, or incorrect screw length. Once the hole enlarges, the effective load-bearing area decreases, which can further reduce clamping force.
Sheet Cracking, Deformation and Local Collapse
Insufficient sheet ductility, excessive forming force, or angled installation can cause cracks and local collapse. For thin-sheet assemblies, edge distance and installation direction are also important design factors.
Chips, Burrs and Screws That Cannot Fully Enter the Assembly
Chips generated by cutting screws may affect thread engagement if they are not evacuated. Excessive burrs can also create gaps between sheets, visible defects, or interference during subsequent assembly.
For applications that require low chip generation, engineers should evaluate a thread-forming solution or add chip-removal and hole-edge inspection steps to the process.
Vibration Loosening and Long-Term Fatigue Failure
Long-term vibration can gradually reduce clamping force at the joint interface. In addition to the screw itself, engineers must consider sheet stiffness, fastener spacing, load direction, and the fatigue characteristics of the overall structure.
Quality Control of Pre-Drilled Holes, Installation Direction and Assembly Process
Stable sheet metal assembly requires control of hole size, hole position, sheet overlap, and screw perpendicularity. In high-volume production, abnormal installation, missing screws, angled installation, and hole-position deviation should also be monitored.
Basic Testing of Pull-Out, Shear and Corrosion Resistance
Quality testing may include pull-out resistance, strip-out resistance, shear performance, and corrosion resistance.
For long-term outdoor applications, material, coating, and service environment should be evaluated together. Screwtrade’s corrosion-resistant coating guide discusses the application characteristics of Ruspert, Dacromet, and zinc-plated coatings.
How to Establish an Engineering Selection Process for Sheet Metal Screws
Identify the Sheet Material, Thickness and Number of Layers
First determine the sheet type, hardness, ductility, total thickness, and number of connected layers. These parameters define the basic range of thread-formation methods and screw lengths.
Determine Whether a Pre-Drilled Hole Is Required
If the production process already includes punching or drilling, engineers should evaluate whether a pre-drilled hole can improve assembly stability. If the goal is to reduce operations, self-drilling screws may be considered, but their drilling capacity must be confirmed against the sheet thickness.
Evaluate Strength, Vibration and Disassembly Requirements
Static joints, vibration-loaded joints, and serviceable joints have different requirements. Engineers should identify the required tensile load, shear load, vibration resistance, and number of disassembly cycles before selecting the thread design.
Compare Thread-Forming and Thread-Cutting Solutions
For ductile sheet where low chip generation and high efficiency are important, thread-forming screws may be evaluated first. For harder materials, specific pre-drilled holes, or applications that require the screw to cut the thread, thread-cutting screws may be more suitable.
Verify Installation Efficiency, Failure Risk and Service Life
Testing should not only confirm whether the screw can be installed. It should also evaluate installation resistance, sheet deformation, thread integrity, repeat disassembly, and the joint condition after long-term vibration.
Confirm the Final Fastening Solution Through Testing
The final solution should be based on tests using the actual material and process conditions. The resulting specification should define hole size, screw length, installation method, and inspection criteria rather than relying only on experience.
If the application requires matching against specific sheet materials, drawings, standards, or volume-production conditions, technical requirements can be submitted through Screwtrade’s Contact Us . The page allows users to provide information such as specifications, standards, coating, washer type, packaging, and quantity requirements.
Development Trends in Sheet Metal Fastening Technology
High-Strength Connections in Thinner Sheet
As lightweight manufacturing expands, the industry needs higher connection strength in thinner sheet. This will drive further optimization of thread geometry, fastener materials, and hole-wall design.
Low-Resistance Thread Designs for Automated Assembly
Automated production requires stable installation resistance, controllable equipment loads, and fewer broken screws, feed failures, and angled installations. Low-resistance designs suited to high-speed assembly will therefore become increasingly important.
Multi-Material Connections and Lightweight Manufacturing
The combined use of steel, aluminum, coated sheet, and composite materials creates additional challenges for metal fastening technology. Future fastening solutions must account for strength, corrosion, and differences in thermal expansion.
Low-Chip, Low-Contamination and Sustainable Production
Reducing chips helps maintain a cleaner production environment and lowers cleaning and waste-disposal costs. Low-contamination manufacturing, material efficiency, and designs that support disassembly will increasingly become part of the sheet metal fastening system.
Digital Monitoring and Quality Traceability of the Connection Process
Sensors, vision inspection, and production-data management can identify installation abnormalities, hole-position deviations, and connection-quality problems in real time. Digital traceability will help manufacturers move from post-process inspection toward process control.
Conclusion: Select the Right Screw According to the Connection Mechanism
Thread-Forming and Thread-Cutting Screws Have No Absolute Winner
Thread-forming screws and thread-cutting screws are suitable for different materials, hole conditions, and manufacturing environments. Their differences should not be reduced to which type is universally superior. The correct decision must be based on the actual connection mechanism.
Proper Selection Depends on Material, Thickness, Hole Type and Assembly Method
Material hardness, sheet thickness, pre-drilled holes, effective thread engagement, joint loading, and disassembly requirements all affect the final result. Only by evaluating these factors together can manufacturers establish a stable sheet metal assembly solution.
Reliable Sheet Metal Connections Require Coordination Between Fastener, Process and Quality Control
Reliable sheet metal fastening is not simply a matter of selecting one screw. It depends on thread design, material compatibility, installation process, process inspection, and service environment.
For manufacturers, establishing a systematic sheet metal fastening standard is essential to improving connection quality and reducing the risk of failure.
Related News
Other news you might be interested in
Why Self-Drilling Screws Fail to Drill: A Substrate and Installation Checklist
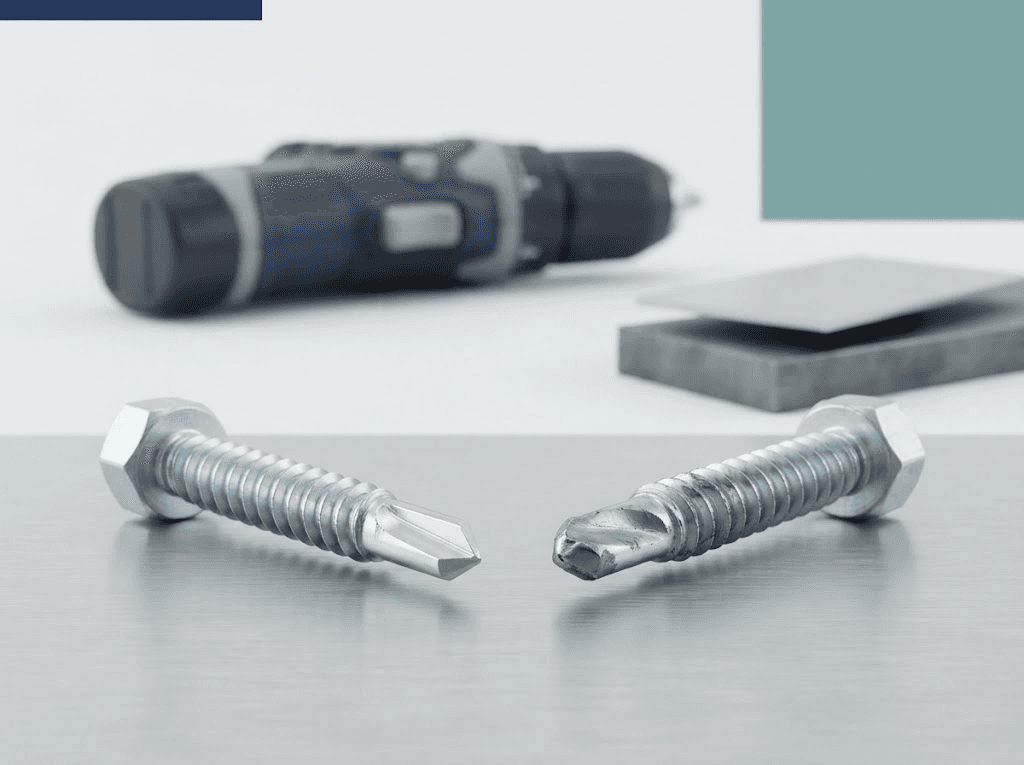
When a self-drilling screw spins against steel without making progress, the purchasing decision becomes urgent: should the installer change the tool settings, should the buyer order a different screw, or should the supplier investigate the batch?A useful diagnosis starts by identifying exactly where drilling stops. Record the material at that point, check the selected screw against the assembly, and then compare installation conditions. This approach gives buyers a clearer basis for deciding what to change and what evidence to request.
Bulk Self-Drilling Screws: An RFQ Checklist for U.S. Importers and Distributors
When sourcing bulk self-drilling screws, a unit price is only useful if you know exactly what it covers. Two quotations may appear to describe the same product while differing in dimensions, coating, packaging, or delivery conditions. For U.S. importers and distributors managing several SKUs, those differences can make supplier comparisons difficult. A clear request for quotation—an RFQ—helps suppliers understand your requirements and gives your purchasing team a consistent basis for reviewing their offers. This checklist explains what to include, which details need confirmation, and how to turn an initial inquiry into a specification that both buyer and supplier can review.
Want to know more?
Get in touch with us for more information about our services and products.